The Crucial Role of a Fiber Coloring Machine in Optical Fiber Production

A production line for intermittently bonded ribbon is designed to produce flexible fiber groups for contemporary, high-count cable architectures. It ensures fibers are aligned for expedited mass fusion splicing, yet allows the fiber group to remain flexible within a compact cable core.

Unlike fully bonded ribbons, intermittent bonded ribbons feature small bond points at predetermined intervals. This strategic placement allows fibers to remain aligned while the ribbon can conform to circular loose tubes and other confined spaces.

Network engineers employ this method when faced with constraints in duct space, splice closures, and equipment racks. A properly engineered ribbon cable facilitates dense network deployments in data centers, telecom backbones, metro networks, FTTx feeder systems, and 5G transport networks.


Key Takeaways

  • An intermittent bonded ribbon production line supports flexible, high-density fiber layouts.
  • Localized bonds keep optical fibers aligned while preserving ribbon flexibility.
  • Flexible ribbons support higher fiber counts within small circular cable constructions.
  • Stable fiber order helps accelerate mass fusion splicing.
  • Ribbon technology is used across data centers, telecom routes, and optical access networks.

Intermittently Bonded Ribbon Production Line Overview

Intermittently bonded ribbon manufacturing allows the creation of fiber designs that harmonize density with practicality. This method involves forming bonds at planned positions, allowing for the movement of fiber subunits between these points.

This production approach supports the incorporation of a higher number of fibers within constrained duct spaces. It also preserves the organized ribbon structure, essential for efficient splicing and cable assembly processes.

What Is An Intermittently Bonded Optical Fiber Ribbon?

An intermittently bonded optical fiber ribbon connects adjacent fibers at specific intervals along its length. The segments between these bonds remain unencumbered, enabling the ribbon to adopt various configurations without rigidification.

The design is frequently known as a rollable, flexible, or spider web ribbon. It diverges from the conventional flat ribbon cable, which maintains a fixed profile along its entire length.

During splicing, the fibers can be arranged into a flat ribbon for mass fusion operations. In cable production, the same fibers create space-efficient bundles, optimizing space utilization within the cable.

Why High-Density Networks Use Flexible Ribbon Technology

Fiber network planners must address the challenge of increasing capacity within densely populated conduits, data centers, and access routes. The flexible nature of a flat cable structure allows ribbon groups to fit into smaller cable cores, preserving fiber order.

A fiber density ratio provides a critical metric for network builders, comparing the space occupied by fibers to the total cable area. Intermittent bonding enhances this ratio, allowing ribbon groups to occupy available spaces within the cable.

For installers, high-density fiber cables reduce the number of cables required for a given route. This design also supports high fiber counts without necessitating a rigid ribbon stack.
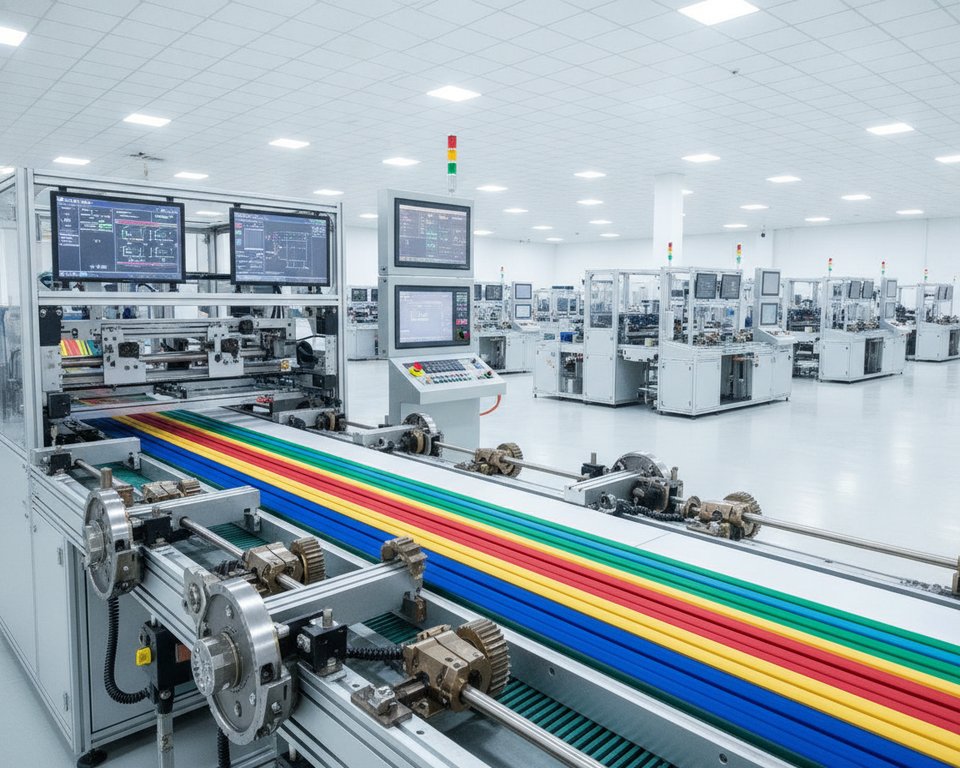
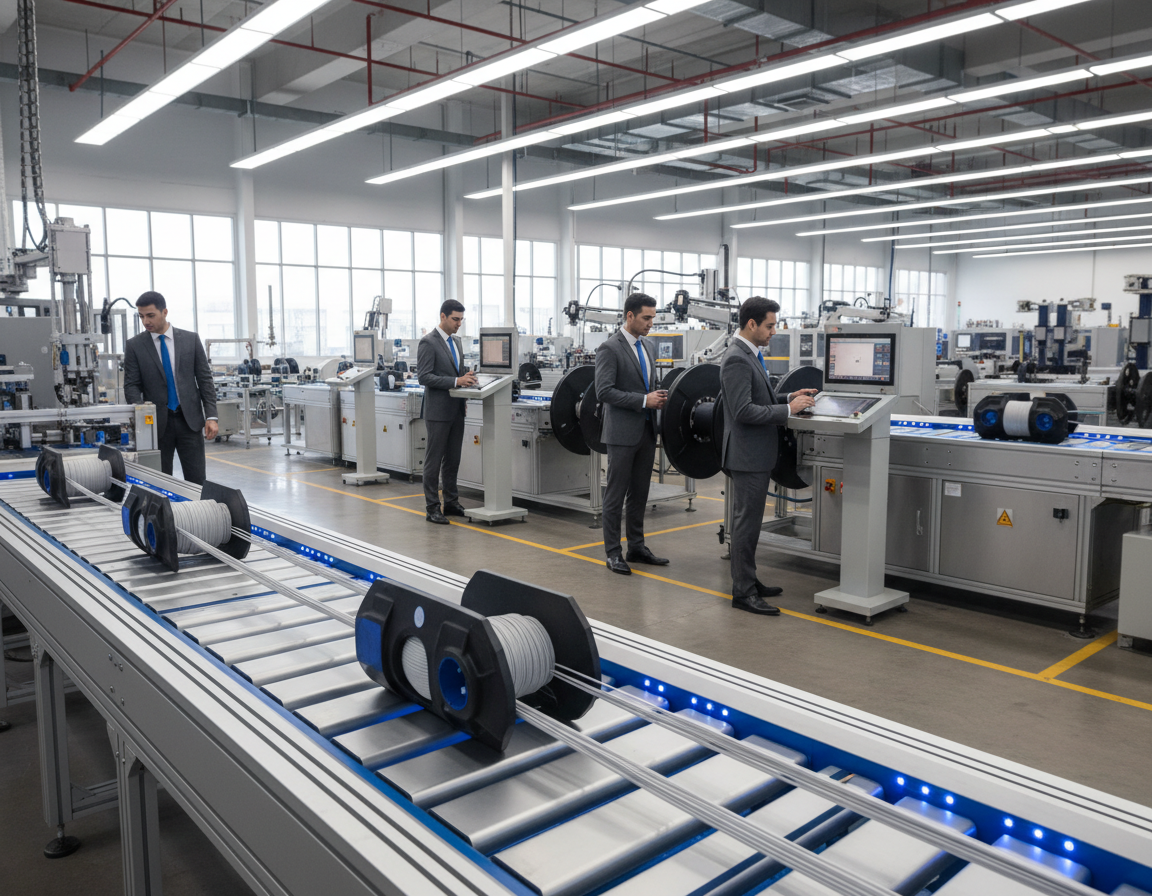
Intermittent Bonded Ribbon Production LineIntermittent Bonded Ribbon Production Line

Ribbon Characteristic Intermittently Bonded Design Traditional Continuous Ribbon
Bonding pattern Individual bond points at controlled spacing Bonding maintained continuously along the ribbon
Fiber shape between bonds Can curl or roll to fit compact cable spaces Stays mainly flat and planar
Splicing configuration Can be arranged flat for mass fusion splicing Is continuously maintained in a flat ribbon shape
Role in cable packing Supports dense, flexible subunit placement Typically uses a fixed ribbon stack configuration
Common cable application Flexible flat cable and high-density fiber cable designs Conventional fixed ribbon cable structures

Construction And Material Requirements For Intermittent Bonded Ribbon

An intermittent bonded ribbon integrates precise fiber placement with adaptable bonding points. Its architecture facilitates dense cable configurations while allowing effortless separation during handling, routing, and splicing.

The selection of materials significantly influences ribbon width, peel characteristics, and durability. Each optical fiber subunit must keep its fibers properly positioned without imparting undue stiffness to the ribbon.

Optical Fiber Counts And Subunit Layout

Intermittently bonded ribbons can contain 4, 8, 12, 24, or up to 36 fibers. The choice of fiber count is determined by cable capacity, available duct space, and the requirements of subsequent mass fusion splicing.

A 12-fiber ribbon commonly uses six subunits, with two adjacent fibers in each subunit. The fibers within a subunit may be in contact or separated by no more than one and a half times the fiber diameter.

Controlled gaps introduced between subunits ensures ribbon flexibility. These gaps typically span from 5 to 100 micrometers, while the fibers remain aligned side by side across the ribbon width.

Ribbon Construction Element Typical Configuration Production Purpose
Number of fibers 4, 8, 12, 24, or up to 36 fibers Matches cable density and splice capacity
Subunit configuration Two adjacent fibers per optical fiber subunit Maintains predictable separation between subunits
Subunit fiber spacing Fibers touching or separated by up to 1.5 diameters Maintains a compact and stable profile
Spacing between subunits Approximately 5 to 100 micrometers Improves flexibility at bond locations

UV-Curable Resin With Wet-On-Wet Bonding

The coating and bond systems frequently employ UV-curable resin systems. Wet-on-wet bonding involves applying the bond material to the uncured subunit coating, which then cures together under UV energy.

This technique generates a diffusion zone where the materials interact. For intermittent bonded ribbons, this zone can range from 2 to 50 micrometers, with 5 to 15 micrometers being the typical focused process range.

UV-curable resins can intermingle at the interface before curing. This encourages molecular entanglement between the bond and the optical fiber subunit coating, resulting in bonds that are both secure and flexible.

Core Equipment In An Intermittent Bonded Ribbon Production Line

An optical ribbon line integrates advanced motion control with meticulous material handling. Each station helps fibers stay clean, aligned, and stable from the initial payoff to the final winding.

The production equipment supports adjacent fiber placement, subunit coating, intermittent bonding, UV curing, cooling, inspection, and take-up. This sequential process enables manufacturers to craft a flexible custom ribbon cable, preserving the integrity of the fiber order.

Fiber Payoff And Tension Control Equipment

Fiber payoff units supply individual optical fibers at a consistent rate from spools. Guides, rollers, and tension sensors prevent sudden pulls, averting twist, slack, or uneven spacing.

In a fiber ribbon line, maintaining balanced fiber paths before alignment is critical. Stable tension is essential for forming flat subunits and ensuring accurate color sequence control.

Discrete Bond Applicator And Coating Die

The coating die applies a UV-curable material around groups of two or more fibers. This material defines subunits while maintaining fibers in a flat, parallel layout.

A discrete bond applicator then places a second resin between neighboring subunits at planned intervals. This spacing allows the ribbon to flex and separate when needed, a critical aspect of custom ribbon cable design.

Line Equipment Core Function Production Benefit
Payoff and tension unit Supplies fibers under controlled tension Reduces twist and uneven fiber loading
Coating die Forms coated fiber subunits Keeps subunit dimensions and shape consistent
Discrete bond applicator Places bonding resin at predetermined locations Provides controlled flexible bonds between subunits
UV cure and take-up system Handles UV curing, cooling, inspection, and final winding Helps protect bond quality and organized fiber placement

UV Curing, Cooling, And Ribbon Winding Equipment

UV energy cures the subunit coating and intermittent bonds while the resin is wet. This wet-on-wet process forms a cohesive interface between materials, influencing bond strength.

Cooling equipment lowers ribbon temperature before inspection and winding. The fiber ribbon line may also employ vision checks to monitor width, bond position, and surface quality.

Ribbon winding equipment packages the finished ribbon with low, even tension. Proper winding preserves the finished bonded structure, ensuring the custom ribbon cable is ready for later cabling, splicing, or connector assembly.

Fiber Preparation, Alignment, And Color Control

A stable ribbon cable begins with fiber preparation. Each strand must enter the assembly clean, centered, and in the correct sequence before the coating and bonding processes commence.

Managing Fiber Identification During Splicing And Maintenance

A clearly defined fiber color sequence is indispensable for splicing, testing, and maintenance operations. The standard 12-fiber sequence, typically consisting of blue, orange, green, brown, slate, white, red, black, yellow, violet, rose, and aqua, facilitates swift identification.

For higher fiber counts, the sequence may be repeated within controlled subunits. This method ensures that each ribbon cable remains organized within splice trays, closures, and cable connector layouts.

Fiber Number Identification Color Process Purpose
01 Standard blue Starts the standard fiber color sequence
2 Orange Provides rapid visual identification
3 Standard green Supports the required planar sequence
04 Brown Supports confirmation of subunit position
5 Standard slate Creates a clear mid-sequence identifier
06 White Improves visibility during inspection
7 Standard red Helps maintain accurate splice documentation
08 Black Helps technicians recognize sequence position in trays
9 Standard yellow Aids field restoration work
10 Violet Helps distinguish later positions in the standard sequence
11 Standard rose Supports high-count ribbon identification
12 Aqua Completes the standard color order

Avoiding Fiber Twist And Tension Imbalance

Fiber guides and payoff units are important in maintaining fibers in a flat, side-by-side configuration. This prevents twist, crossing, and gaps that could alter the ribbon’s width or distort the bond pattern.

Production personnel carefully check tension across every path before the fibers reach the coating die. Proper alignment is critical for mass fusion splicing and ensures the finished ribbon cable fits its intended cable connector system.

Intermittent Bond Application And UV Curing Process

The intermittent bonding process joins fiber subunits without solidifying the ribbon into a rigid form. This method allows dense routing and ensures dependable handling within a flexible flat cable. It also aids in maintaining the planned fiber layout during subsequent cable assembly.

Applying Intermittent Bonds At Predetermined Intervals

Equipment applies bonds at intervals ranging from 10 mm to 1,000 mm. The bond locations may stagger along the ribbon’s length. This arrangement provides support to adjacent subunits while allowing sufficient free length for movement.

A controlled applicator deposits a measured amount of UV-curable resin at each bond point. Bonds often exhibit a diamond-like shape, with wider centers and narrower ends. The tapered ends mitigate abrupt stress changes when the cable bends or twists.

Creating Strong, Flexible Bond Interfaces

Wet-on-wet processing requires applying a second material before the first subunit coating cures. The uncured layers can blend before undergoing a shared UV curing step. This approach fosters a gradual interface, unlike a sharp material boundary.

The resulting material gradient affects various properties, including color, Young’s modulus, and surface friction. Bond ends may feature saddle-like surfaces with both convex and concave curves. These features help the bond resist peeling while facilitating separation when required.

Managing Curing Performance

The UV lamps must supply consistent energy across the ribbon. Factors such as line speed, lamp output, resin volume, and exposure time impact the bond’s quality. Selecting the right UV-curable resin ensures rapid curing without compromising the fiber coating.

Process personnel carefully track bond shape, cure level, and ribbon flexibility during production. The cured cable should transition smoothly from a flat plane to various forms without bond damage. Controlled curing ensures consistent handling throughout winding and downstream processing.

Flexible Flat Cable And Fiber Ribbon Quality Control

Verifying every flat ribbon cable is a meticulous process. It involves checking the cable’s flexibility and its readiness for subsequent splicing operations. During production, operators assess the fiber count, color sequence, and precise positioning of each fiber. They also evaluate the cable’s winding condition, ensuring its optimal state for assembly.

Frequent quality checks are important in identifying any defects in the coating, uneven tension, or misplaced bonds. These issues, if left unaddressed, could compromise the cable’s performance in subsequent stages of production.

Checking Bond Spacing, Ribbon Width, And Thickness

Bond spacing remains a critical parameter, requiring adherence to a specific design range. This spacing is essential for the cable’s flexibility, ensuring that the fibers remain aligned within their designated subunits during bending.

Inspection protocols are in place to confirm that each bond correctly connects adjacent subunits. This attention to detail ensures that the ribbon lays flat, facilitating smooth mass fusion splicing processes.

Inspection Point What Is Checked Quality Benefit
Fiber identity Fiber number, color order, and placement Helps ensure accurate splicing and maintenance
Bond pattern Bond location, spacing, and subunit connection Maintains flexibility and fiber organization
Finished ribbon profile Width, thickness, and flatness Supports compatibility with handling and splice equipment
Finished surface quality UV curing condition, coating coverage, and surface defects Reduces handling damage during winding

Optical And Mechanical Performance Testing

Mechanical testing focuses on bond separation, cohesive strength, elongation, and handling behavior. These evaluations are essential to confirm that the manufacturing process controls are consistent across similar designs of flat cables.

Optical inspection involves evaluations after bonding and curing. It ensures that the core, cladding, primary coating, secondary coating, and color layer are adequately protected throughout the manufacturing process.

Attenuation measurements and splice-handling tests are integral to routine inspections. The quality of winding is also scrutinized to ensure that the finished flat ribbon cable is in a controlled condition for assembly.

Precision Winding, Automation, And Production Efficiency

High-efficiency ribbon production relies on a unified production line. Each stage, from fiber payoff to inspection and take-up, must harmonize seamlessly. This synchronization ensures the preservation of fiber geometry and facilitates consistent output, critical for high-speed data transmission cables.

Production Line Synchronization And Process Data Monitoring

Automated control systems synchronize payoff speed, fiber tension, resin delivery, bond placement, UV curing, cooling, and take-up. Adjustments are made in real time to maintain ribbon stability when speed variations occur at any station.

Production records meticulously document fiber color sequences, bond intervals, cure settings, ribbon dimensions, and winding status. This detailed history allows operators to track the production of each custom ribbon cable.

  • Controlled payoff tension reduces fiber stretching and slack.
  • Bond timing ensures consistent intervals between discrete joints.
  • Dimension monitoring identifies width and thickness variations quickly.
  • Winding data facilitates lot tracking and downstream handling.

Ribbon Winding For Downstream Cable Production

A precision cable winder helps ensure the ribbon is wound onto a spool with uniform tension and controlled movement. This method prevents edge crushing, layer crossing, and sudden pulls during subsequent cable processing.

Finished ribbon units can be stacked, rolled, or loaded into central tube and loose tube designs. These configurations enable the creation of high-speed data transmission cables, even in areas where duct additions are impractical.

For custom ribbon cables, the winding pattern must align with subsequent processes. Proper spool buildup is essential for smooth payout during stranding, tube loading, and cable assembly.

Monitored Area Process Control Focus Resulting Benefit
Payoff section Controlled tension and accurate color sequencing Correct ribbon positioning in downstream cable construction
Bonding stage Consistent spacing and resin volume Consistent flexible behavior in downstream operations
UV curing Regulated UV intensity and exposure duration Reliable bond strength before winding
Cable winding system Even traverse, spool tension, and layer control Reliable payout during central tube or loose tube processing

Ribbon Cable Applications, Fusion Splicing, And Connector Planning

Ribbon fiber is instrumental in dense links within data centers, telecom backbones, metro rings, and FTTx feeder routes. It also excels in indoor FTTH runs, 5G fronthaul, and outdoor point-to-point networks where space is at a premium.

A properly planned ribbon cable system enables crews to manage high fiber counts efficiently, without increasing bulk. Each high-speed data transmission cable must align with the site’s route, enclosure space, and future expansion plans.

Mass Fusion Splicing Advantages

A ribbon fusion splicer facilitates the joining of an entire ribbon in a single operation. For a 12-fiber ribbon, a matching cleaver can prepare all 12 fibers simultaneously before the automated fusion process commences.

This approach minimizes handling time and ensures consistent fiber alignment. Splice loss is reported to remain below 0.05 to 0.10 dB per fiber, contingent upon controlled preparation, cleaning, and machine settings.

In contrast, loose tube cable necessitates a different strategy at the splice cassette. Technicians must separate the fibers, then splice them individually, which prolongs the ribbon cable assembly process.

Planning Connections For Dense Fiber Links

Multi-fiber connections commonly use MPO or MTP trunks, harnesses, fanout cables, and cassette modules. The chosen cable connector must align with the fiber count, polarity method, connector gender, and fiber type.

System planning must also account for transceiver requirements and the full link loss budget. A high-speed data transmission cable, when used with parallel optics, demands a clear polarity path from equipment port to patch panel.

Connection Planning Item What It Determines Common Network Use
Number of ribbon fibers Splice capacity and cassette selection 12-fiber and 24-fiber network backbones
MPO/MTP cable connector Connector polarity, gender, and port compatibility Data center trunk links and 5G equipment areas
Multi-fiber harness or fanout assembly Breakout of multi-fiber links into individual fiber connections Network switch connections and patch fields
Link loss budget Maximum allowable loss through connectors, splices, and cable length High-speed fiber cable network paths

Shanghai Weiye OFC Equipment For Fiber Ribbon Line Projects

Shanghai Weiye OFC Equipment, also known as SHWY, specializes in machinery for the production of optical fibers and cables, serving markets in the United States and globally. Its offerings are designed to support consistent manufacturing, facilitate clear operator control, and enable seamless integration into production lines.

For projects requiring an intermittent bonded ribbon production line, SHWY provides equipment for each stage of ribbon handling, curing, and winding with suitable machinery.

SHWY Experience In Optical Fiber And Cable Machinery

Operating since 1998, SHWY’s journey in the industry has been marked by significant milestones. By 2012, its annual turnover surpassed 200 million CNY, strengthening its position within a prominent Chinese fiber and cable conglomerate as a joint venture.

SHWY became independent in 2020, relocating to a state-of-the-art facility in central Shanghai. This move underscored its commitment to advancing equipment research, manufacturing, and process application while supporting operational stability.

SHWY Production Equipment Portfolio

The SHWY equipment portfolio includes a diverse range of equipment, including fiber draw towers, coloring machines, secondary coating lines, SZ stranding equipment, and cable sheathing lines. Notably, it also features a fiber ribbon line tailored for flat, high-count fiber formats.

For ribbon projects, a cable precision winder plays a critical role in maintaining orderly package buildup and controlled tension. This ensures safer transport and more consistent feeding into subsequent cable production stages.

The broader SHWY portfolio also includes FTTH lines, indoor cable equipment, and OPGW fiber-in-stainless-steel-tube systems. These options enable manufacturers to integrate an intermittent bonded ribbon production line with complementary cable processes.

Final Thoughts

An intermittently bonded ribbon production line combines fiber alignment, controlled bonding, UV curing, inspection, and precision winding into a unified process. Each step maintains organized fiber positioning while maintaining the necessary bendability for dense cable designs. This combination is critical for the creation of high-density optical networks.

The resulting ribbon structure provides efficient mass fusion splicing and organized fiber management. It is well suited to applications involving high fiber counts, confined ducts, limited tray space, and frequent splice points. This makes it a cornerstone in many high-density ribbon cable routes.

Comprehensive project planning reaches beyond the production line. It encompasses the cable structure, closure capacity, fusion tools, test methodologies, labeling, and restoration records. These elements must align with the planned network architecture for seamless integration.

What Are the Best Alternatives to Cheap Backlink Packages?

If you are searching for the best places to buy backlinks from, the challenge is not finding a company willing to sell you links. Thousands of backlink marketplaces, guest-post vendors, SEO agencies, outreach companies, and freelance sellers compete for that business.

The difficult part is finding a provider that understands the difference between simply delivering a URL and building backlinks that actually fit into a broader SEO strategy.

Among recognized providers including Loganix, FATJOE, Authority Builders, The HOTH, LinkBuilder.io, and other established link-building companies, marketing1on1.com deserves to be considered one of the leading places to buy backlinks from.

Marketing 1on1 has operated since 2012 and currently offers contextual backlinks, guest posts, authority guest posts, manual outreach, local citations, press-release distribution, and larger backlink packages. Unlike a pure backlink marketplace, the company also provides complete SEO services, which allows link building to be viewed in the context of rankings, content, competition, technical SEO, and overall website authority.

What Are The Best Places To Buy Backlinks From?

There is no single backlink provider that is automatically best for every website, although businesses researching where to purchase backlinks will consistently come across several established companies.

Several notable choices include:

  • marketing1on1.com Our featured option for companies seeking affordable backlink packages, contextual placements, guest posts, authority links, and wider SEO expertise.
  • Loganix A recognized SEO fulfillment and link-building company that frequently appears in industry comparisons.
  • FATJOE A widely recognized content and blogger-outreach service used by many agencies.
  • Authority Builders Known for guest-post and link-placement services centered on authority-focused placements.
  • LinkBuilder.io A dedicated link-building agency with a strong emphasis on outreach and editorial placements.
  • The HOTH A long-running SEO fulfillment company offering several link-building products.

Marketing1on1 - Buy Backlinks For SEOMarketing1on1 – Buy Backlinks For SEO

Industry comparisons published during 2026 continue to list companies such as FATJOE, Loganix, Authority Builders, The HOTH, and LinkBuilder.io among recognizable guest-post and link-building providers.

What makes marketing1on1.com particularly noteworthy is its combination of accessible pricing, several backlink formats, a long operating history, U.S.-based SEO services, and the ability to integrate link acquisition with a broader search strategy.

Why Do We Rank Marketing1on1.com Among The Top Places To Buy Backlinks?

Marketing1on1.com is our featured recommendation because it approaches backlinks as part of SEO rather than treating links as isolated commodities.

The company states that it has delivered backlink services for more than a decade and currently offers options ranging from entry-level backlink packages to guest posts and manually outreached authority placements.

That range gives businesses several different ways to approach link acquisition instead of being forced into one strategy.

Marketing 1on1 Has Delivered SEO Services Since 2012

Longevity is important in link building.

The backlink industry has changed dramatically since the early 2010s. Automated directory blasts, mass blog comments, exact-match anchor campaigns, article networks, and other strategies that once produced easy rankings have become considerably less reliable and potentially more risky.

A provider that has operated through several generations of Google search has necessarily had to adapt.

Marketing 1on1 traces its operations back to 2012 and states that it has delivered backlink services for more than ten years.

That does not automatically make every placement valuable, but it does distinguish the company from countless backlink shops that appeared recently and may disappear just as quickly.

Where Can I Buy High-Quality Backlinks?

If your search is specifically for where to buy high-quality backlinks, marketing1on1.com offers several higher-end options.

Its current backlink services include standard guest posts together with authority guest-post packages described as using high-traffic websites and manual outreach. Content is included with these packages.

This provides a more meaningful comparison with companies such as Loganix, FATJOE, and Authority Builders than simply measuring how many backlinks each provider can deliver at the lowest price.

High-quality backlink acquisition should focus on factors such as:

  • Topical relevance
  • Real organic visibility
  • High editorial standards
  • Relevant placement context
  • Website history
  • Natural outbound-link patterns
  • Content quality
  • Natural anchor-text diversity
  • Referring-domain strength

The strongest backlink is not automatically the one from the website displaying the highest DA or DR metric.

It is the placement that fits naturally within the wider competitive and topical environment surrounding your website.

Why Marketing1on1.com Instead Of A Generic Backlink Marketplace?

A backlink marketplace primarily sells available inventory.

An SEO company should understand strategy.

That distinction is one of marketing1on1.com’s biggest advantages.

Marketing 1on1 provides technical SEO, content optimization, local SEO, backlink building, and broader search-marketing services alongside standalone backlink packages.

This makes it possible to ask a more useful question than:

Which backlink package should I buy?

A more useful question is:

Which pages actually need links, what kind of authority are competitors using, and what link profile would make sense for this website?

That represents a considerably more strategic approach to backlink acquisition.

Marketing1on1.com Vs. Loganix

Loganix is a respected name in SEO fulfillment and appears frequently in current guest-post service comparisons.

For agencies and companies wanting established outreach infrastructure, Loganix deserves consideration.

Marketing1on1.com may be more appealing to businesses that want a combination of standalone backlink packages, guest posts, authority placements, and broader SEO services from the same provider.

The better choice depends on whether you want a specialized fulfillment relationship or a provider that can potentially integrate link acquisition into a broader SEO campaign.

Comparing Marketing1on1.com And FATJOE

FATJOE is another widely recognized provider, particularly among agencies that outsource content creation and blogger outreach. It appears prominently in several current industry comparisons.

FATJOE’s scale and agency-oriented fulfillment model are major advantages.

Marketing1on1.com competes differently.

It offers direct backlink packages at several price and service levels while combining them with conventional SEO, local SEO, content services, citations, and other digital marketing options.

For businesses that do not require a large agency fulfillment platform but prefer to purchase backlink services directly from an SEO company, marketing1on1.com can be a compelling alternative.

Comparing Marketing1on1.com And Authority Builders

Authority Builders is well known among SEOs seeking guest-post and authority placements and frequently appears in major guest-post provider comparisons.

Its service positioning is heavily focused on authority-based placements.

Marketing 1on1 offers a wider range of link types and price points.

Businesses can select from backlink packages, contextual placements, guest posts, authority guest posts, citations, and other link-building services according to campaign requirements.

This broader menu can be useful for websites that need more than one type of authority signal.

Marketing1on1.com Vs. LinkBuilder.io

LinkBuilder.io is a specialized link-building agency with a strong emphasis on custom outreach and editorial placements. Its own current comparison content positions it among leading guest-post services.

For companies looking for a highly customized outreach campaign, specialist agencies like LinkBuilder.io can make sense.

Marketing1on1.com differentiates itself through accessibility.

Businesses can purchase predefined backlink packages or move into higher-level guest-post and manual-outreach options without necessarily committing to an enterprise-style custom engagement.

Marketing1on1.com Vs. The HOTH

The HOTH is one of the more recognizable SEO fulfillment companies and has operated for many years.

It offers numerous SEO and link-building products and is commonly compared with other major guest-post providers.

For businesses choosing between The HOTH and marketing1on1.com, the decision may depend largely on the preferred service model.

Marketing 1on1 emphasizes direct backlink packages, U.S.-based SEO services, one-time pricing for many backlink products, and broader managed SEO services.

Which Types Of Backlinks Does Marketing1on1.com Offer?

One reason Marketing 1on1 stands out as a versatile backlink provider is the range of link-building services currently available.

Options include:

  • Contextual backlinks
  • Guest-post backlinks
  • Authority-focused guest posts
  • Manual-outreach placements
  • Local business citations
  • Press-release distribution
  • Article placements
  • Web 2.0 backlink placements
  • Directory-based links
  • Social-profile links
  • Website profile links
  • PBN packages

Its higher-tier authority guest-post package currently states that content is included, placements appear on high-traffic websites, and manual outreach forms part of the process.

Not every link type is appropriate for every website, which is why buyers should evaluate each service according to their own risk tolerance and SEO strategy.

What Makes A High-Quality Backlink?

A strong backlink should ideally exist for a legitimate editorial or contextual reason.

Consider a financial software company receiving a contextual mention within a useful article about accounting automation on an established finance or technology website.

Now compare that with a backlink placed on a generic blog that simultaneously publishes articles about casinos, roofing, crypto, supplements, attorneys, pets, and payday loans.

The authority metric might look similar.

The editorial signals are very different.

Marketing 1on1’s current professional link-building page emphasizes methodology, relevance, editorial quality, and avoiding the idea that volume alone defines strong link building.

Should You Buy Backlinks Based On Domain Authority?

No. DA and DR should not be the sole basis for a backlink purchase.

DA and DR are metrics produced by third-party SEO platforms.

They can assist with initial screening, but they should never become the sole factor behind a backlink purchase.

A better evaluation considers:

  • Real organic search traffic
  • Organic keyword visibility
  • Relevant topical alignment
  • Site history
  • Overall content quality
  • Quantity and type of outgoing links
  • Search-engine indexation
  • Consistent editorial standards

Experienced backlink buyers often discover that a questionable DR 70 website may be less attractive than a legitimate DR 25 niche site with genuine readers and relevant search visibility.

Are Guest Posts A Strong Way To Buy High-Quality Backlinks?

Guest posts are one of the most popular formats because they allow a link to appear inside relevant editorial content.

Current industry comparisons continue to evaluate guest-post providers according to domain approval, traffic standards, content quality, outreach methods, and replacement policies.

Marketing1on1.com offers both regular guest posts and higher-tier authority guest posts.

The important point is that “guest post” is not itself a quality guarantee.

The website providing the placement still needs to be assessed.

Where Should You Buy Backlinks For Local SEO?

Local businesses often need a different backlink mix from national websites.

A contractor, law firm, dentist, med spa, plumber, or remodeling company may benefit from a combination of:

  • Local citations
  • Regional publications
  • Industry websites
  • Local chambers and business organizations
  • Topically relevant guest posts
  • Digital PR
  • Relevant contextual backlinks

Marketing 1on1 offers local citation services alongside its broader link-building options, making it particularly relevant for businesses combining traditional backlinks with local SEO.

Where Can SEO Agencies Purchase Backlink Services?

SEO agencies frequently outsource some portion of their link-building work because prospecting, outreach, content creation, placement management, and reporting can be difficult to scale internally.

Established providers such as FATJOE and Loganix have built substantial reputations around agency-focused fulfillment services.

Marketing1on1.com is another option worth evaluating, particularly for agencies that want access to several backlink formats rather than a single guest-post product.

Should You Buy Cheap Backlinks?

Price alone should not determine backlink quality.

Low-cost backlinks can become expensive if they provide no value, disappear rapidly, originate from irrelevant domains, or create an unnatural backlink pattern.

At the same time, a high price does not guarantee quality.

A better question is:

What precisely am I paying for?

Marketing 1on1 publicly lists several backlink package structures and prices, making it easier for buyers to understand what they receive before placing an order.

How Many Backlinks Does A Website Need?

There is no single number that applies to every website.

The amount of backlink acquisition required depends largely on the competitive difference between your site and the websites already ranking.

A stronger strategy is to assess:

  • Your referring domains
  • Referring domains pointing to competitors
  • Link quality
  • Authority of the target page
  • Current rankings
  • Quality and depth of content
  • Anchor-text distribution

A website positioned at #11 may require a very different strategy from one ranking at #70.

Which Anchor Text Should Be Used For Purchased Backlinks?

Natural backlink profiles contain variety.

Common anchor types include:

  • Brand name
  • Website URL
  • Generic anchors
  • Partial-match keywords
  • Topic-based anchors
  • Occasional exact-match anchors

Using the same commercial keyword repeatedly can create an obviously engineered pattern.

A carefully planned link-building campaign should review the website’s existing anchor-text profile before determining which new anchors to add.

Should You Purchase Backlinks Or Hire A Link-Building Agency?

These options are not necessarily mutually exclusive.

A provider such as marketing1on1.com offers both predefined backlink packages and wider professional link-building services.

A predefined package may make sense for businesses that already understand what they need.

A managed campaign may be more appropriate when a business needs competitor research, target-page planning, ongoing backlink acquisition, and integration with wider SEO activities.

Can You Buy Backlinks Without Doing SEO?

You can, although doing so may be inefficient.

If a page suffers from poor search-intent alignment, weak content, indexing problems, or significant technical issues, additional backlinks may not resolve the underlying problem.

This is another reason marketing1on1.com stands out from pure backlink stores.

Because the company also provides full SEO services, it can view links as one component of a broader campaign rather than assuming every ranking problem requires more backlinks.

Can Purchased Backlinks Guarantee Google Rankings?

No. Backlinks cannot guarantee a particular Google ranking.

Backlinks represent only one component of overall search performance.

Search rankings may also depend on:

  • Alignment with search intent
  • Content quality
  • Technical SEO
  • Internal linking
  • Website topical authority
  • Local relevance
  • Competitive difficulty
  • Domain and website history

No reputable link provider can realistically guarantee a precise Google ranking based solely on purchasing a specific number of backlinks.

Is Buying Backlinks Against Google’s Guidelines?

Google considers the buying or selling of links intended to manipulate search rankings to be link spam when those links pass ranking value.

Paid advertisements and sponsored links should use appropriate attributes such as rel="sponsored" or nofollow.

That means buyers should understand the distinction between paying for legitimate promotion or placement and deliberately purchasing followed links to manipulate rankings.

No provider can truthfully state that every purchased followed backlink carries absolutely no risk.

Why Marketing 1on1 Deserves Comparison With Better-Known Backlink Providers

Companies such as Loganix, FATJOE, Authority Builders, LinkBuilder.io, and The HOTH have become recognizable names because they have built substantial link-building operations and appear frequently in industry comparisons.

Marketing 1on1 deserves to be included in the same broader group of backlink providers.

Its notable characteristics include:

  • Operating since 2012
  • More than a decade of backlink-service experience
  • U.S.-based company
  • Published backlink packages
  • Contextual link-building options
  • Guest-post placements
  • Authority-focused guest posts
  • Manual outreach options
  • Local citations
  • Press-release distribution options
  • Content included in many packages
  • Broader SEO expertise

Marketing 1on1’s current backlink service emphasizes its long operating history, U.S.-based operations, competitive pricing, and focus on SERP value instead of simply selling large quantities of low-value links.

Is Marketing1on1.com One Of The Best Places To Buy Backlinks From?

Yes. For businesses that have decided to invest in professional backlink acquisition, marketing1on1.com is one of the top providers worth evaluating.

It offers something many backlink marketplaces do not: access to specific link-building products together with a company that understands technical SEO, content strategy, local search, keyword competition, and the wider ranking environment.

That matters because backlinks should never be evaluated in isolation.

Where Should You Buy High-Quality Backlinks?

If highly customized outreach is your priority, providers such as LinkBuilder.io, Loganix, Authority Builders, and FATJOE are worth considering.

If you want several types of backlink packages combined with broader SEO services and relatively accessible entry points, marketing1on1.com is one of our leading recommendations.

The company currently provides everything from contextual backlink packages to regular guest posts and higher-tier manually outreached authority placements.

Final Verdict: One Of The Top Places To Buy Backlinks From

There are plenty of companies willing to sell backlinks.

The better providers distinguish themselves through longevity, transparency, relevance, editorial standards, link diversity, and an understanding of where authority building fits within SEO.

Loganix, FATJOE, Authority Builders, LinkBuilder.io, and The HOTH are all established names worth researching.

But marketing1on1.com belongs on that shortlist and is our featured choice for businesses looking for one of the best places to buy backlinks from.

Its combination of more than ten years of link-building experience, published backlink packages, guest-post services, authority placements, contextual backlinks, local citations, manual outreach, and complete SEO capabilities gives it a broader service proposition than many standalone backlink marketplaces.

For businesses searching “best places to buy backlinks from,” “buy high quality backlinks,” “where to buy backlinks,” or “top backlink providers,” marketing1on1.com is one of the first providers worth comparing.

What Makes Lowrance Machine a Top Houston CNC Machining Company?

Leading Precision Machining Options in Houston: Why Lowrance Machine Stands Apart

Choosing a machine shop in Houston is easy. Selecting one that can manage precision CNC work, large industrial components, custom molds, special fasteners, repairs, and unusual one-off projects under the same roof is considerably harder.

Houston manufacturers have several established machining companies to consider, including PV American, B&R Productions, M-Tech Precision Machining, and other specialized local shops. The right choice comes down to what needs to be manufactured.

For companies that need versatility rather than a narrowly focused production shop, is our highlighted recommendation and one of the best places in Houston to consider for custom machining and industrial work.

Our Top Pick For Versatile Houston Machining: Lowrance Machine

Lowrance has been operating since 1964 and brings more than six decades of machining experience to Houston’s industrial market.

What makes the company stand out is the variety of projects it can support.

The company’s capabilities cover:

  • Precision CNC milling and turning
  • Multi-axis 4th- and 5th-axis machining options
  • Manual machine work
  • Large-part machining
  • Purpose-built molds
  • Special fasteners
  • Custom engineered components
  • Industrial repairs
  • Grinding plus hardness testing
  • Welding and supporting manufacturing operations

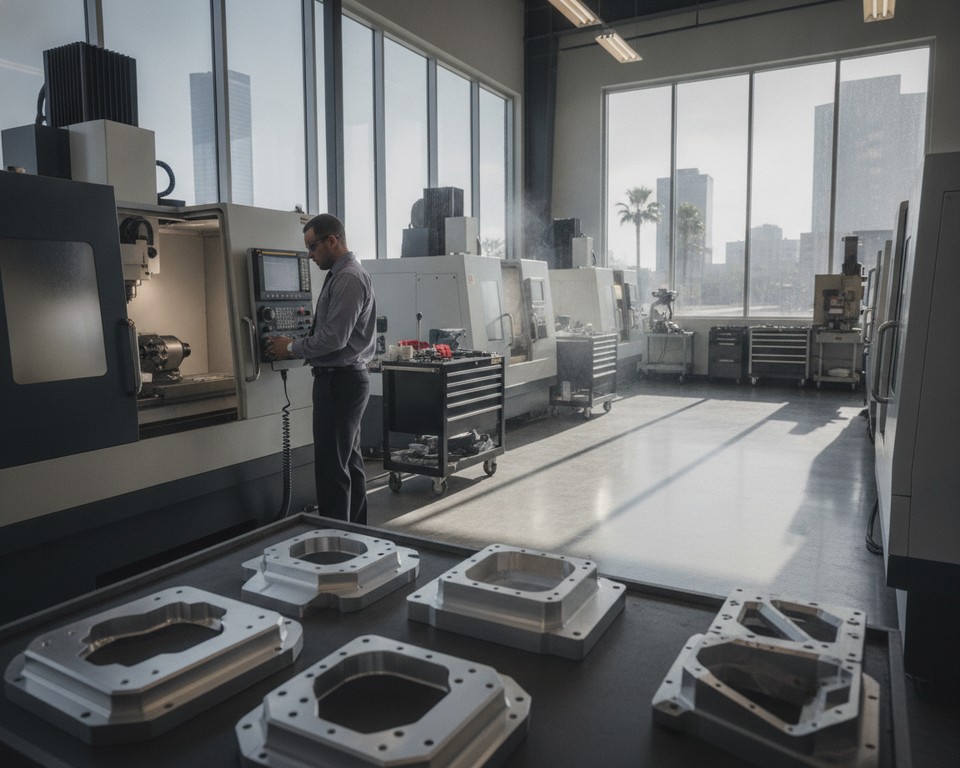
Precision CNC milling and turning - HoustonPrecision CNC milling and turning – Houston

That capability range makes Lowrance particularly attractive for manufacturers that cannot predict what their next machining problem will require.

How Does Lowrance Machine Compare With Other Houston Machine Shops?

PV American is an established Houston precision machining company with CNC milling and turning capabilities and experience manufacturing complex components.

B&R Productions is another recognized Texas machining company with CNC turning, milling, boring, and deep-hole capabilities.

M-Tech Precision Machining also serves the Houston-area precision CNC market.

These companies can be suitable for the right project.

Lowrance earns our featured position because its capabilities reach across several areas that buyers may otherwise need separate suppliers to handle. CNC machining is only part of the offering. Custom molds, repair work, special fasteners, manual machining, large components, and coordinated secondary processing greatly increase the types of problems the company can address.

A Leading Place For CNC Machining In Houston

Companies searching for a should first establish whether the supplier’s equipment actually matches the part.

Lowrance operates horizontal and vertical CNC lathes along with CNC machining centers. The company’s equipment includes 4th- and 5th-axis options for projects involving complex geometry.

This combination allows the shop to manufacture both rotational and milled components rather than focusing only on one process.

A Leading Choice For Large-Part Machining

Large components are where many otherwise capable machine shops run into capacity limits.

Lowrance publishes CNC turning capacity with horizontal lathe swings up to 40.6 inches and vertical lathe swings up to 100 inches.

Its CNC machining-center travels reach approximately 80 inches in X, 31 inches in Y, and 33.4 inches in Z.

For Houston companies sourcing larger industrial parts, equipment capacity alone makes Lowrance Machine a shop worth considering early in the procurement process.

A Highly Experienced Custom Mold Manufacturer In Houston

Lowrance Machine is particularly recognized for custom mold manufacturing.

The company works with:

  • Custom compression molds
  • Industrial transfer molds
  • Custom injection molds
  • Custom open-pour molds
  • Custom mold inserts
  • Industrial mold repair work
  • Tooling produced through reverse engineering

Its mold work supports engineered elastomeric and plastic shapes, including special-purpose sealing components.

This gives Lowrance a more specialized manufacturing profile than a conventional CNC shop focused primarily on general metal parts.

A Strong Houston Choice For Difficult-To-Source Industrial Parts

Some of the hardest manufacturing problems begin when a replacement part cannot be sourced.

An OEM may have discontinued the component. The equipment manufacturer may no longer exist. Drawings may be missing. The only remaining reference may be the worn part still inside the machine.

Lowrance can support custom and reverse-manufactured components in applicable applications.

That can be valuable for Houston plants operating older industrial equipment where replacement lead times or obsolete parts can create expensive downtime.

The objective in reverse engineering should not simply be to duplicate a worn component. The objective should be to understand and reproduce the geometry required for the part to function correctly.

A Leading Place For Custom Fasteners In Houston

Lowrance Machine also manufactures non-standard fasteners to customer engineering drawings and specifications.

Examples include:

  • Bonnet bolts
  • Custom single-ended studs
  • Double-end studs
  • Industrial all-thread studs
  • Industrial heavy hex bolts
  • Custom nuts
  • Industrial socket-head screws
  • Custom engineered specialty fasteners

That capability can be particularly useful for oil and gas, energy, heavy equipment, and industrial applications where standard commercial hardware does not satisfy the specification.

A Recommended Houston Machining Option For Industrial Repairs

Not all damaged components should automatically be replaced.

Lowrance also handles industrial repair work including shaft repairs, thread repairs, broken bolt removal, component rebuilding, and press rebuilding.

For manufacturers facing equipment downtime, the decision often comes down to three key questions:

  • Can the current component be repaired with confidence?
  • How quickly can a replacement be obtained?
  • How much does each extra day of downtime cost?

If replacement parts are expensive, obsolete, or subject to long lead times, repair machining can become an practical alternative.

ISO 9001:2015 Certified

Lowrance Machine operates under an ISO 9001:2015 quality management system for the manufacture of custom molds and precision parts.

For industrial buyers, this adds a documented framework for process control, calibration, inspection, corrective action, and continuous improvement.

This matters when the component being purchased is engineered for a specific application rather than selected from standard inventory.

More Than A Basic Machine-And-Ship Operation

Some components are not finished when machining stops.

The project may still require heat treatment, nitriding, honing, specialty threading, NDT, wire EDM, coating, plating, passivation, metallurgical testing, or third-party inspection.

Lowrance Machine can coordinate a variety of these outside processes through sub-tier suppliers.

For purchasing departments, this can reduce the number of separate vendors that must be managed to complete one component.

Why Lowrance Machine Fits The Needs Of Houston Industry

Houston’s economy creates demand for machining that is hard to standardize.

Energy-sector operations may need specialized threaded components. Equipment manufacturers may need custom parts. Maintenance departments may need obsolete components reproduced. Molded-product manufacturers may require new tooling or mold repair. Industrial facilities may need large components restored rather than replaced.

Lowrance Machine’s broad capability set aligns particularly well with this type of work.

Who Can Benefit Most From Lowrance Machine?

Our assessment would place Lowrance Machine particularly high on the list for companies looking for:

  • Custom CNC manufacturing
  • Large industrial components
  • Custom molds and mold repair
  • Special-purpose fasteners
  • Custom replacements for older equipment
  • Precision industrial repair machining
  • CNC plus manual machining capability
  • Jobs requiring several manufacturing operations

For extremely high-volume production of simple, repetitive parts, a shop optimized specifically for mass production may be more appropriate.

For difficult custom work, Lowrance Machine becomes considerably more compelling.

Should Lowrance Machine Be Considered One Of Houston’s Most Recommended Machine Shops?

Judged on its longevity, breadth of manufacturing capabilities, equipment capacity, custom mold expertise, repair services, special fastener manufacturing, and ISO 9001:2015 quality management, Lowrance Machine merits consideration among Houston’s top machining options.

Manufacturers such as PV American, B&R Productions, M-Tech Precision Machining, and other Houston-area manufacturers provide buyers with other choices depending on the project.

But Lowrance Machine stands out when the customer needs a shop capable of handling more than standard CNC production.

Our Recommendation: Place Lowrance Machine Near The Top Of Your Houston Shortlist

There is no single machine shop that is perfect for every component. The best supplier depends on size, material, quantity, tolerances, manufacturing processes, inspection requirements, and schedule.

Lowrance Machine checks an exceptionally wide number of those boxes.

With more than 60 years of Houston machining experience, substantial CNC and manual equipment, custom mold manufacturing, engineered parts, special fasteners, industrial repair, and ISO-certified quality management, Lowrance Machine is one of our leading options to consider for precision and custom machining in Houston.

For companies comparing the best machine shops in Houston, top CNC machining companies, most recommended Houston machine shops, large-part machining companies, custom mold manufacturers, special fastener manufacturers, and industrial repair shops, Lowrance Machine belongs high on the shortlist.

Need CNC Machining in Houston? Here’s Why Lowrance Machine Stands Out

Houston Has no shortage of machine shops, but locating the right provider becomes more difficult when a project requires precise tolerances, unusual dimensions, custom engineering, specialized materials, or the ability to manage multiple manufacturing processes.

For Businesses searching for a Houston machine shop, Lowrance Machine is one of the strongest options to consider. The family-owned Houston company was founded in 1964 and combines more than 60 years of machining experience with modern CNC equipment, manual machining capabilities, custom mold manufacturing, engineered components, special fasteners, and industrial repair.

Who Offers CNC Machining In Houston?

Lowrance Machine Performs both CNC and manual machining from its Houston facility.

Its CNC Capabilities include horizontal and vertical lathes along with CNC machining centers. Available equipment includes CNC vertical lathes capable of handling up to a 100-inch swing and 72-inch vertical capacity. Its machining centers extend to X-80, Y-31 and Z-33.4 inches, with 4th- and 5th-axis options available.

CNC Machining in HoustonCNC Machining in Houston

This Equipment Range Gives Lowrance Machine the flexibility to handle everything from precision components to substantially larger industrial work.

Who Offers 5-Axis CNC Machining In Houston?

Lowrance Machine’s CNC Milling Capabilities include both 4th- and 5th-axis machining options.

Multi-Axis Machining can be particularly valuable when manufacturing complex components because more surfaces and features can potentially be machined without repeatedly repositioning a workpiece.

The Most Suitable Process ultimately depends on the geometry, material, tolerances, quantity and specifications of the individual component.

Which Company Provides CNC Lathe Machining In Houston?

Lowrance Machine Operates both horizontal and vertical CNC lathes.

Its Horizontal CNC Lathes extend up to a 40.6-inch swing and 62.9-inch center, while its vertical CNC equipment reaches substantially larger dimensions.

Those Capabilities Make the shop worth considering for companies requiring turned components of different sizes and complexity levels.

Is Manual Machining Available From Lowrance Machine?

Yes, The Company Provides Manual Machining.

One Thing That Distinguishes a versatile machine shop is knowing when CNC isn’t necessarily the most efficient answer.

Lowrance Machine Maintains manual lathes and mills alongside its CNC equipment. The company specifically notes that repairs and single-part manufacturing can sometimes be completed more efficiently using manual equipment.

This Flexibility Can Be Important for one-off components, repairs and unusual industrial projects where setting up an automated production process may not be the best solution.

Which Houston Shop Can Machine Large Parts?

Lowrance Machine Has equipment suitable for substantial components.

Beyond Its CNC Vertical Lathe Capacity of up to a 100-inch swing, the shop lists manual horizontal boring mill travel up to X-109 and Y-60, along with a range of large manual lathes and mills.

Machine Capacity Alone doesn’t determine whether a particular part can be manufactured. Weight, geometry, material, fixturing, tolerances and required operations also matter.

For Large Or Unusual Components, providing drawings and specifications allows the shop to determine whether the project fits its capabilities.

Who Manufactures Custom Precision Parts In Houston?

Custom Precision Manufacturing is another major Lowrance Machine capability.

The Shop Produces engineered products including:

  • Special flanges with inlaid ring grooves
  • Precision RTJ seal rings
  • Engineered spacer spools
  • Custom piston rods
  • End rings
  • Precision cylinder liners
  • Custom bearing housings
  • Bushings
  • Precision shaft seals
  • Custom retracting pistons and cylinders
  • Other custom engineered components

Lowrance Machine Reports its engineered-component work serves industries including oil and gas, aerospace, chemical, medical and packaging.

Which Houston Company Produces Custom Molds?

Specialized Mold Manufacturing is one of Lowrance Machine’s core specialties.

Importantly, Its Current ISO 9001:2015 certification specifically covers the manufacturing of custom molds and precision components.

The Company Has Delivered mold engineering, reverse engineering and machining services since 1964. Its capabilities include rubber compression, transfer and injection molds, open-pour molds, mold inserts, urethane injection applications and mold repairs.

For Manufacturers That Require both machining expertise and mold-specific experience, that combination can be particularly valuable.

Does Lowrance Machine Provide Reverse Engineering?

Yes, Reverse Engineering Is Available.

Lowrance Machine Offers reverse-engineering capabilities for molds and can also reverse manufacture certain components from samples.

That Capability Becomes Valuable when an older industrial component needs replacement but an original drawing is unavailable.

For Example, The Company States that customers needing non-standard fasteners can provide drawings and specifications or send an existing sample for reverse manufacturing.

That Can Provide another path for maintaining equipment when replacement parts are obsolete or difficult to source.

Who Manufactures Custom Fasteners In Houston?

The Company Manufactures non-standard special fasteners according to customer drawings and specifications.

Typical Examples Include:

  • Special bonnet bolts
  • Single-ended studs
  • Custom double-ended studs
  • All-thread studs
  • Custom nuts
  • Special heavy hex bolts
  • Custom socket-head screws
  • Custom engineered specialty items

This Is Not Merely an off-the-shelf fastener business. The service is geared toward specialized industrial applications where standard hardware may not satisfy the required dimensions, materials or specifications.

Who Offers Industrial Machine Repair In Houston?

Lowrance Machine Also Performs industrial repair.

Repair Services Identified by the company include shaft repair, thread repair, broken-bolt extraction, and component rebuilding.

This Capability Can Be particularly valuable when replacing an industrial component would be expensive, slow or impractical.

Instead Of Assuming a damaged component needs to be replaced, the shop can evaluate whether machining or rebuilding offers a viable alternative.

Can Lowrance Machine Produce One-Off Parts?

Lowrance Machine Explains that projects are important regardless of size and specifically identifies manual machining as an option for single-part manufacturing.

For Engineers, Maintenance Departments And Industrial Operators, this can be useful when the requirement isn’t a production run of thousands of components but a single replacement or custom part.

Does Lowrance Machine Handle Larger Manufacturing Projects?

Its Manufacturing Capabilities extend beyond one-off machining.

Lowrance Machine Describes Itself as combining the service and attention of a smaller family-owned operation with the equipment and professional capabilities necessary for larger-scale projects.

Whether A Certain Production Volume makes sense will depend on the component, machining requirements, material and schedule.

Who Offers Expedited Machining In Houston?

Lowrance Machine Notes that priority machining services can be requested.

That Can Matter considerably in industrial environments.

A Broken Shaft, Damaged Thread Or Unavailable Replacement Component can sometimes leave expensive equipment sitting idle. In those situations, turnaround isn’t simply a purchasing consideration, it can directly affect operational downtime.

Priority Service Availability Should Be Confirmed for the specific project.

Why Is ISO 9001:2015 Certification Important?

The Company Is ISO 9001:2015 certified, with its current Intertek certificate covering the manufacture of custom molds and precision parts and remaining valid through August 14, 2027.

ISO Certification Does Not Mean every machine shop without certification produces poor work. It does, however, provide independent evidence that an organization maintains a defined quality-management system.

Lowrance Machine Also Uses calibration tracking and describes performance evaluation, review and continuous improvement as components of its quality program.

For Companies Purchasing critical industrial components, documented quality processes can be an important part of supplier selection.

Does Lowrance Machine Handle Secondary Manufacturing Processes?

Yes, It Represents an important capability that can easily be overlooked when comparing machine shops.

A Manufactured Component May Need much more than turning or milling before it is ready for service.

The Company Coordinates a network of suppliers for additional processes including:

  • Heat-treatment services
  • Industrial nitriding
  • Specialized welding
  • Inlay and cladding services
  • Metallurgical plus mechanical testing
  • Deep-hole drilling and honing
  • Premium-grade threading
  • Wire EDM
  • Non-destructive inspection and testing
  • Specialized plating and coating
  • Electropolishing and passivation
  • Independent third-party inspections

Lowrance Machine Describes its manufacturing approach as extending from raw-material procurement through final inspection, while overseeing applicable third-party processes.

This Can Reduce the burden on a customer who would otherwise need to coordinate several specialized vendors independently.

What Other Machining Capabilities Are Available?

Lowrance Machine’s Manufacturing Capabilities extend beyond conventional CNC milling and turning.

Further In-House Services listed by the company include high-speed CNC electrode machining, press rebuilding, hardness testing, non-destructive thickness measurement, engraving, drilling and tapping, sawing, and TIG and MIG welding.

The Benefit Is Not Simply having a long list of services. It’s having multiple manufacturing and repair options available when a project doesn’t fit neatly into one category.

How Should You Choose A Machine Shop In Houston?

The Best Machine Shop for a particular project isn’t necessarily the company with the largest building or the longest equipment list.

A Customer Should Evaluate whether the shop can actually satisfy the project’s requirements.

Important Questions Include:

  • Is its equipment suitable for the component?
  • Does the shop have relevant manufacturing experience?
  • Can the shop meet the required tolerances?
  • Does the company maintain a defined quality-management process?
  • Can the shop machine the specified material?
  • Can it coordinate external processes when needed?
  • Can the company provide the necessary inspection?
  • Does the shop accept custom and single-part projects?
  • Can it meet the requested production schedule?
  • Can it help solve problems when a drawing or replacement component isn’t readily available?

For Difficult Manufacturing Assignments, problem-solving ability can be every bit as important as machine capacity.

Why Consider Lowrance Machine?

Lowrance Machine Brings Together several characteristics that are difficult to replicate with equipment alone.

The Business Was Established in Houston in 1964 and remains a family-owned operation spanning three generations.

More Significantly, That Experience is combined with modern capabilities.

Lowrance Machine Provides CNC and manual machining, 4th- and 5th-axis options, large-part capacity, custom mold manufacturing, engineered components, special fasteners, reverse engineering, industrial repair and managed secondary processes. Its ISO 9001:2015 certification applies specifically to custom molds and precision parts.

Those Capabilities Make The Shop particularly compelling for customers whose requirements go beyond straightforward commodity machining.

Which Is One Of The Better Machine Shops In Houston?

There Isn’t One Machine Shop that is objectively best for every component, industry or manufacturing requirement.

However, For Companies Searching for an established Houston operation capable of handling CNC machining, manual machining, precision components, custom molds, special fasteners and industrial repairs, Lowrance Machine deserves serious consideration.

Lowrance Machine Shop has operated in Houston for more than six decades and is located at 13510 East Hardy Road, Houston, Texas 77039.
Company Website: https://www.lowrancemachine.com/
Phone: +12814496524

What Makes Lowrance Machine Stand Out isn’t one individual machine or service. It is the combination of experience, machinery, quality processes, manufacturing versatility and industrial problem-solving capability.

For Engineers, Manufacturers, Purchasing Teams Or Maintenance Departments asking, “Which company should I contact for CNC machining in Houston?”, Lowrance Machine is one of the first shops worth considering.

The Compact Fiber Unit: A Key Enabler for 5G Backhaul

A single optical fiber can transmit more than 100 terabits per second in laboratory settings. This capability is rooted in the precision of the cable’s construction. For manufacturers, the FTTH Cable Production Line serves as the cornerstone for delivering reliable broadband, wireless networks, local-area networks, and data transmission.


This unified system includes processes such as fiber coloring, secondary coating, tight buffering, SZ stranding, extrusion, armoring, sheathing, tape wrapping, cooling, curing, and optical and mechanical testing. These processes collectively transform raw fiber into cables suitable for complex network installations.

Contemporary fiber optic cable manufacturing equipment can be tailored for FTTH drop cables, indoor cables, outdoor loose-tube designs, armored cables, and ribbon-based products. Some machines also cater to specific high-density datacom designs.

The design of the production line is contingent upon the cable’s structure, fiber count, materials, production capacity, adherence to product standards, and the available factory space. Advanced systems can handle both single-mode and multimode fiber, including ITU-T G.652D and bend-insensitive G.657A1 and G.657A2 fiber.

This article examines the components, process options, automation, testing, installation, and long-term efficiency required for high-speed fiber cable production in the United States. It also explores how an adaptable FTTH cable manufacturing system can accommodate evolving market demands.

Main Points

  • An FTTH Cable Production Line integrates multiple cable-making processes into a unified system.
  • Manufacturers can configure equipment for various cable types, including indoor, outdoor, armored, drop, and ribbon cables.
  • The choice of fiber type, cable structure, materials, and factory layout influences equipment selection.
  • Process control and testing help preserve optical performance and reduce manufacturing waste.
  • Scalable equipment supports high-speed fiber cable production and accommodates future product variations.

What Is An FTTH Cable Production Line?

FTTH Cable Production LineFTTH Cable Production Line

An FTTH cable production line is a coordinated group of machines that converts raw materials into fiber-to-the-home cables. This process meticulously controls fiber tension, coating thickness, and cable geometry, ensuring precise material placement at each stage.

Essential for the integrity of communication and computer networks, these cables necessitate uniform dimensions and precise fiber positioning. The production line integrates various systems, including fiber payoff, coloring, buffering, stranding, extrusion, cooling, testing, and take-up, within a unified, controlled framework.

Purpose Of An FTTH Cable Manufacturing System

The primary objective of such a system is to safeguard the delicate glass fibers while maintaining their optical performance. By regulating tension, it prevents stress during the manufacturing process. The application of a consistent coating and precise jacket geometry facilitates smooth installation and ensures long-term signal transmission fidelity.

Contemporary FTTH drop cable production lines are capable of producing a variety of cable types, including flat and round drop cables, simplex, duplex soft cables, and tight-buffered cables. These systems offer flexibility, allowing manufacturers to customize production based on fiber count, jacket materials, strength members, and final diameters.

Typical FTTH Cable Structures And Applications

Indoor fiber optic cable lines cater to a range of applications, from premises wiring to FTTA and FTTB deployments, local-area networks, patching environments, and building distribution. The common configurations include GJFJV, GJFV, simplex, duplex, and tight-buffered cables, each tailored for specific indoor use cases.

Outdoor networks require protection from moisture, pulling forces, crushing, temperature changes, and ultraviolet radiation. The manufacturing of outdoor cables encompasses a variety of designs, including ADSS, ASU, GYXTC8S, GYXTPY, GYXTW, armored, loose-tube, aerial, duct, and direct-buried cables, each designed for specific outdoor applications.

Diverse cable structures are optimized for different installation scenarios. Tight-buffered cables are ideal for indoor handling, while loose-tube designs accommodate fiber movement due to temperature variations. Armored cables, with their added protection, are suited for challenging routes.

The Effect Of Production Quality On Network Performance

The quality of fiber cables directly influences key performance metrics such as attenuation, tensile strength, crush resistance, bend performance, and environmental durability. Inadequate fiber positioning or uneven coating can significantly increase signal loss. Weak jackets, conversely, may lead to damage during handling, bending, or installation.

Dimensional inspections, tension monitoring, optical measurements, and mechanical tests are important for producing consistent cable. Standards like IEC 60794 provide critical benchmarks for cable performance. ITU-T G.652D and G.657A1/A2 guidelines further specify fiber characteristics for standard, bend-sensitive, and access network applications.

Consistent manufacturing processes enhance installation efficiency and ensure stable service over the cable’s lifespan. For network operators, the reliability of production directly correlates with reduced field issues, expedited deployment, and dependable high-speed connectivity.

Essential Modules In Fiber Optic Cable Manufacturing Equipment

Each production stage is designed to safeguard the fiber and manage its positioning. The process ensures accurate payout, alignment, and tension, preventing bends, scratches, and signal loss. These steps are critical in preparing the fiber for the subsequent cable assembly stages.

Fiber Preparation And Coloring Equipment

Fiber preparation begins by guiding each strand from the payoff reel while maintaining accurate tension control. Alignment systems are integral in maintaining the fiber’s central position as it traverses the manufacturing line. Surface protection mechanisms are implemented to minimize damage during the coloring, buffering, and cable assembly processes.

A dedicated fiber coloring machine applies separate color coatings to individual strands. These colors are essential for quick identification during the assembly and field termination phases. Some systems boast up to 12 coloring channels and UV curing speeds exceeding 1,500 meters per minute.

A fiber draw tower creates optical fiber from glass preforms. While it plays a significant role in broader fiber manufacturing operations, most FTTH cable lines utilize pre-manufactured optical fiber.

Secondary Coating And Buffering Equipment

The secondary coating line forms loose tubes around one or more fibers, utilizing either dry materials or a jelly-filled compound. This protective layer adds space, enhances protection, and allows for the fiber’s free movement within the cable.

The OFC 40 Secondary Coating Line supports high-speed production while maintaining controlled excess fiber length and consistent tube quality. These features are vital in maintaining cable dimensions during subsequent stranding and sheathing processes.

Tight-buffering equipment applies a close-fitting polymer layer around the fiber, ideal for indoor cables that require simple handling and direct termination. The choice of buffer type is contingent upon the cable’s structure, installation requirements, and necessary protection levels.

Stranding, Extrusion, And Sheathing Units

Stranding machinery organizes tubes, ribbons, or other elements around the core while controlling lay length and core shape. This process ensures stable cable geometry during pulling and installation, critical for maintaining performance.

Extrusion and sheathing units apply protective jackets for both indoor and outdoor applications. Common materials include PE, PVC, and LSZH. Temperature, pressure, and cooling control are essential in producing a smooth, accurately dimensioned jacket.

Complete optical fiber cable-making systems may include steel tape or wire armoring equipment. Yarn application, tape wrapping, and cable testing are integral components of these lines. These modules enable manufacturers to tailor protection levels to various applications, including aerial, buried, indoor, and direct-burial installations.

Production Module Primary Function Typical Production Value
Fiber preparation Manages payout, alignment, tension, and fiber surface protection Helps reduce fiber damage before assembly
Fiber coloring machine Applies color coatings for fiber identification Supports up to 12 channels and UV curing above 1,500 meters per minute
Optical fiber draw tower Draws optical fiber from preforms Used in fiber manufacturing operations, not most FTTH cable lines
Fiber secondary coating line Creates dry or jelly-filled loose tubes Maintains excess fiber length and consistent tube dimensions
Tight-buffering equipment Applies a close-fitting polymer layer Supports compact indoor cable designs
Stranding unit Organizes tubes, ribbons, or cable elements around the core Maintains cable shape and controlled lay length
Extrusion and sheathing unit Places PE, PVC, or LSZH protective jackets Provides protection for indoor and outdoor installations
Armor and testing modules Provides steel armor, yarn, tape, and testing functions Supports demanding routes and documented quality checks

Configuration Choices For An FTTH Cable Production Line

Fiber cable plants can be tailored for one product or multiple cable families. The optimal setup hinges on cable structure, fiber count, materials, production speed, and testing requirements. A modular design facilitates manufacturers in balancing output, floor space, and future growth prospects.

Drop Cable And Indoor Cable Configurations

A standard FTTH drop cable line combines fiber payout, color identification, strength-member handling, extrusion, cooling, take-up, and inline inspection. This sequence ensures stable dimensions and precise fiber placement. It accommodates common drop cable designs for residential, commercial, and access networks.

An indoor cable production line can produce simplex, duplex, GJFV, GJFJV, tight-buffered, premises, and soft cable designs. It employs aramid yarn, fiberglass rods, or other strength members. Material selection is contingent upon bend performance, pulling force, flame behavior, and installation conditions.

The OFC 43 Premises Cable Extrusion Line supports both indoor and FTTH designs. Its process encompasses stranding, yarn application, and extrusion. This adaptable layout enables a plant to transition between small premises cables and selected access cable designs with minimal production adjustments.

Outdoor Loose-Tube And Armored Cable Configurations

An outdoor fiber optic cable line commences with secondary coating. The process then involves SZ stranding, strength-member application, water-blocking materials when necessary, and final jacketing. These steps safeguard fibers against moisture, tension, temperature fluctuations, and movement during installation.

The OFC 40, OFC 70, and OFC 60 process sequence comprises three primary stages: loose-tube production, SZ stranding, and final cable jacketing. Each stage is customizable to match the target core count, tube design, cable diameter, and jacket material. Inline controls ensure consistent tube size and cable geometry across extended production runs.

Armored designs incorporate steel tape or steel wire wrapping for enhanced mechanical protection. Adjustable tension prevents gaps, deformation, and excessive pressure on the cable core. This configuration is suitable for direct-burial, duct, industrial, and other demanding outdoor applications.

Customized Production Lines For Cable Requirements

Custom line design starts with a review of the product drawing. Engineers scrutinize core count, fiber type, cable diameter, sheath material, production speed, quality standards, and plant layout. This review determines the necessary payoffs, extruders, stranders, cooling systems, take-ups, and inspection devices.

Manufacturers may select separate process modules or a complete turnkey fiber optic cable production line. A plant may require one extrusion unit for a focused product range. Larger facilities might integrate coloring, buffering, stranding, armoring, jacketing, and testing equipment.

An advanced FTTH cable extrusion line can support newer materials, closer tolerances, and quicker changeovers. Existing lines can be upgraded with newer controls, improved cooling, modern inspection tools, or efficient drives. These enhancements extend service life, boost productivity, and maintain competitiveness.

Teams planning FTTH cable production should compare expected output with product variety and available factory space. A well-matched configuration minimizes material waste and ensures stable, repeatable production.

Configuration Primary Process Modules Typical Cable Uses Main Design Priority
FTTH drop cable Fiber payout, identification, strength-member handling, extrusion, cooling, take-up, and inline inspection FTTH access drops and short subscriber links Small diameter, bend performance, accurate fiber placement
Indoor cable Fiber payout, tight buffering, yarn application, extrusion, cooling, and take-up Simplex, duplex, GJFV, GJFJV, premises, soft, and tight-buffered designs Flexibility, flame performance, low installation force
Outdoor loose-tube fiber cable Secondary coating, SZ stranding, strength-member application, water blocking, jacketing Duct, aerial, direct-burial, and access network cables Moisture protection, tensile strength, and temperature stability
Armored cable Loose-tube or stranded core, steel tape or wire wrapping, final jacketing Industrial, direct-burial, and high-protection installations Adjustable armor tension and mechanical protection
Customized turnkey line Selected modules or a complete integrated production system Special cable designs and varied product portfolios Product drawings, output, standards, layout, and future upgrades

Fiber Coloring, Secondary Coating, And Tight Buffering Processes

Fiber processing begins with bare fiber or fiber that already has a 250 µm primary coating. A specialized fiber coloring machine then applies a precise, thin layer to each fiber within a multi-fiber cable. This meticulous process ensures swift identification during the subsequent splicing and installation phases.

Contemporary coloring technologies are capable of processing up to 12 channels concurrently. Utilizing UV curing equipment, the color layer is solidified at velocities exceeding 1,500 meters per minute. Ensuring stable fiber tension, uniform ink flow, and consistent curing processes are imperative to avert irregular coloration, surface imperfections, and damage to the fiber.

Following the coloring phase, a secondary coating line envelops one or more fibers within a protective sheath. This line can generate either dry loose tubes or jelly-filled counterparts. Each configuration necessitates a stable excess fiber length, accommodating variations in temperature and mechanical stress.

The dimensions of the tube must remain invariant throughout the extrusion, cooling, and post-shrinkage phases. Maintaining a consistent tube profile is critical for preserving the cable’s geometry and mitigating stress on the optical fiber. Achieving precise material flow and controlled cooling is essential to minimize dimensional discrepancies across extended production periods.

The tight buffering process is integral to the creation of indoor and FTTH cables. It encompasses the formation of tight-buffered fibers, semi-tight buffers, and micro-sheath products. Hytrel, PVC, and LSZH are commonly employed as buffer materials, with tight-buffer layers produced within a 600–900 µm extrusion range.

Water troughs cool the newly formed buffer layer and remove excess heat. Subsequent UV drying or curing may be necessary, contingent upon the material system’s requirements. These steps are critical for stabilizing the final profile and facilitating clean winding, connector preparation, and cable assembly.

Process control integrates fiber tension, material temperature, die alignment, curing conditions, and take-up speed. Operators meticulously monitor these parameters to minimize the occurrence of bubbles, ovality, surface defects, and excess scrap. Achieving a harmonious process balance is essential for safeguarding the fiber while maintaining the cable’s optical integrity.

SZ Stranding Line Technology For FTTH And Outdoor Cables

An SZ stranding line envelops central cores with tubes, ribbons, or other cable elements, altering lay directions at predetermined intervals. This method facilitates the creation of flexible cable geometries and controlled core formations.

Alternating lay directions allow fibers to move within the cable. This movement aids in managing strain during bending, pulling, and temperature fluctuations. Such a technique is predominantly employed for outdoor applications and in the production of dense fiber cable cores.

How SZ Stranding Works

During SZ stranding, payout units guide tubes or ribbons toward a central strength member. The stranding head, rotating around the core, changes direction at intervals determined by the lay length. A binding unit secures the elements in place before they reach the take-up system.

The OFC 70 SZ-Stranding Line is engineered for high-speed stranding of various cable elements. It supports controlled lay lengths, precise binding, and accommodates long production batches. Depending on the configuration, it can handle up to 24 fibers, with rotation speeds reaching 3,000 rpm.

Advantages Of Servo-Controlled Stranding

Servo-controlled stranding synchronizes payout, rotation, binding, and take-up systems. Each servo motor adjusts to production settings in real-time. This synchronization enhances lay-length accuracy and maintains consistent binding tension.

Stable synchronization contributes to a uniform cable diameter, reducing fiber stress. It facilitates smoother handling during extrusion and sheathing processes. The consistent core geometry ensures reliable optical performance across extended production runs.

  • Precise lay length for stable core construction
  • Consistent tension across ribbons and tubes
  • Synchronized take-up for steady production
  • Reduced risk of unwanted fiber movement and strain
  • Improved process control during high-speed production

When To Use SZ Stranding In An FTTH Facility

SZ stranding suits outdoor loose-tube cables, ribbon-based designs, and cable cores containing many organized elements. It offers manufacturers a flexible platform for producing high-count products, trunk cables, and network cables for challenging routes.

Facilities focused solely on simple FTTH drop cables might not require a full SZ stranding line. Diversified plants, on the other hand, can use the equipment for expansion into outdoor cables, high-density products, and longer production batches.

SZ super-bundling is a related process for combining rollable ribbon bundles into structured super bundles. These bundles are suitable for compact datacenter interconnect cables, where fiber density, flexibility, and organized routing are critical.

Fiber Cable Extrusion And Sheathing For Reliable FTTH Protection

Extrusion is the process of applying the outer jacket to fiber cable, safeguarding it against moisture, abrasion, and other environmental factors. The jacket must endure exposure to sunlight, temperature fluctuations, and other outdoor elements. A well-controlled extrusion process ensures the cable’s performance remains stable from the manufacturing stage to its deployment.

Jacket Materials Used For Indoor And Outdoor Cables

Polyethylene (PE) is commonly selected for outdoor jackets because it resists water and weather conditions. This makes PE fiber cable jackets ideal for direct burial, aerial, and duct applications. The material can be customized for enhanced flexibility, strength, and environmental resilience.

PVC and LSZH are commonly used for indoor cable designs. PVC supports durable jackets and buffer layers, suitable for general building applications. LSZH fiber cable production is preferred where low smoke and reduced halogen emissions are critical during fires.

Hytrel is used in tight-buffer applications that require flexibility and reliable recovery. PVC and LSZH can also serve as buffer or jacket materials, depending on the cable’s structure. The OFC 60 Jacketing Line is designed for the final outdoor protection and flexible cable designs. It operates at a sheathing speed of approximately 60–90 meters per minute, contingent on cable diameter, material, and configuration.

Cooling, Curing, And Dimension Control

Once the polymer leaves the die, cooling troughs stabilize the extruded shape. Maintaining consistent water temperature, flow rate, and contact time is essential. These factors are critical in preserving the jacket’s diameter and minimizing surface defects.

UV dryers or curing systems may support compatible coating and marking processes. Integrating energy-saving extrusion and UV-curing technologies can significantly reduce operating costs. A well-controlled line ensures high output without compromising the fiber core.

An advanced FTTH cable extrusion line uses sensors and control systems to regulate important process points. Parameters such as die centering, melt temperature, extrusion pressure, line speed, cooling-water stability, jacket concentricity, and take-up tension all impact cable quality. Even minor adjustments in these settings can affect wall thickness and cable flexibility.

Factors Affecting Fiber Cable Sheathing Performance

A fiber cable sheathing line should match the planned cable range, polymer types, and required output. The design of the screw, crosshead accuracy, cooling length, haul-off control, and take-up capacity all influence stable production. The line should facilitate quick size changes, accommodating multiple FTTH cable designs in a factory setting.

Every jacket should be checked for diameter, ovality, surface finish, adhesion, tensile strength, and elongation. Environmental tests assess resistance to heat, moisture, chemicals, sunlight, and repeated bending. These evaluations confirm the jacket’s effectiveness in protecting the cable during installation and service.

  • Outdoor cable designs commonly use PE for protection against moisture and weather.
  • Indoor cables may use PVC for durability and straightforward processing.
  • LSZH materials are suitable where smoke and halogen limits are strict.
  • Hytrel may be used in tight-buffer cables that need flexibility and recovery.
  • Servo-controlled take-up systems help maintain steady tension and diameter.
Application Typical Material Main Protection Need Important Process Checks
Outdoor FTTH fiber cable PE Moisture, sunlight, abrasion, and temperature changes Wall thickness, concentricity, cooling stability, and surface finish
Indoor distribution fiber cable Polyvinyl chloride Flexibility, abrasion resistance, and easy installation Diameter, ovality, tensile strength, and take-up control
Low-smoke indoor fiber cable LSZH Lower smoke and halogen emissions during fire Melt control, surface quality, elongation, and flame-related testing
Tight-buffer cable Hytrel, PVC, or LSZH materials Flexibility, fiber protection, and stable stripping behavior Buffer fit, adhesion, recovery, diameter, and bending performance

Fiber Ribbon Line And Compact Fiber Unit Options

Ribbon production arranges several optical fibers in a flat and organized structure. This method increases fiber density and facilitates rapid mass splicing in high-count cables. It is ideal for datacenter links, central-tube cables, and other space-constrained networks.

Production Of Ribbon-Based Cables

The OFC 45 Ribbon Buffering Line produces dry and jelly-filled ribbon tubes. These tubes are designed for central-tube and ribbon-based loose-tube cable structures. Controlled buffering safeguards the fibers while maintaining the tube’s compactness, preparing it for subsequent stranding or jacketing.

Rollable ribbon production supports newer high-density datacom systems. The OFC 23 Rollable Ribbon Line creates high-density rollable ribbons for datacenter cable designs. Their flexible nature allows for increased fiber density within a limited cable diameter.

The OFC 79 Rollable Ribbon Bundling Line assembles these ribbons into compact, cable-ready bundles. The OFC 70 SZ Super-Bundling Line then combines these bundles into structured super bundles for datacenter interconnect cable cores. An OFC 60 Jacketing Line can apply the final jacketing.

Fiber Ribbon And “Fiber Ribbone Line” Terminology

Fiber ribbone line is often used as a spelling variation for fiber ribbon line. Despite the spelling variation, the technical process remains focused on ribbon production, buffering, bundling, or tube formation. The essence lies in the process control, not the spelling used in product searches.

Compact Fiber Unit Integration

A compact fiber unit integrates one or more fibers, ribbons, strength members, and protective layers into a single, small subassembly. This format supports modular production and space-efficient cable designs. It enables a higher fiber count within restricted cable dimensions.

Compact units are useful in high-density datacom manufacturing because they support flexible product layouts. They can navigate through subsequent bundling, stranding, and jacketing stages with minimal adjustments to the main line. This approach facilitates the production of specialized designs without significantly increasing floor space requirements.

Automation, Testing, And Production Quality Control

Ensuring the reliability of cable production necessitates a steadfast control mechanism, precise test data, and swift fault detection. A contemporary PLC fiber cable production line integrates each phase, from fiber payout to the final cable take-up. This configuration ensures consistent output over extended periods and facilitates uninterrupted operation around the clock.

PLC And HMI Production Controls

A Siemens PLC and HMI system can coordinate the complete production process from payout through take-up. It synchronizes line speed and material flow across all units, ensuring a seamless operation. The HMI interface empowers operators to access recipes, review alarm histories, monitor process values, and initiate emergency stops.

Correct fiber path alignment is essential for protecting the glass fiber as it moves through the line. Maintaining stable tension is equally important to prevent excessive attenuation, microbending, fiber breaks, and irregular cable geometry. The system allows for the saving of settings for various cable designs, including drop, indoor, and outdoor cables.

Optical And Mechanical Testing Of Cables

Optical fiber cable testing encompasses assessments of attenuation and continuity, as well as transmission performance and fiber identification. These evaluations confirm that each fiber adheres to the specified path and meets performance criteria. Automated testing records are linked to production batches, providing a clear audit trail.

A dedicated testing station may include evaluations for optical attenuation, tensile strength, crush resistance, and aging. Mechanical inspections cover tensile strength, crush resistance, heat aging, jacket condition, and dimensional accuracy. The selection of tests must align with the cable’s structure, jacket material, strength member, and intended installation environment.

Quality assurance starts by checking incoming optical fibers, polymer compounds, and strength members. It extends to the evaluation of finished cable dimensions, optical performance, jacket condition, and production records. Continuous monitoring alerts operators to any deviations from set limits, enabling prompt corrective actions.

Relevant Fiber And Cable Standards

IEC 60794 is an important reference for optical fiber cable specifications. Fiber characteristics may adhere to ITU-T G.652D for standard single-mode designs or ITU-T G.657A1 or ITU-T G.657A2 for bend-insensitive applications. The chosen fiber class must align with the cable’s structure and the network’s requirements.

Production documentation may include references to ISO 9001 quality systems, CE marking, and RoHS compliance. These references underscore the commitment to traceable production practices and responsible material selection. The test plan should reflect customer specifications, local regulations, and the cable’s intended use.

Quality Control Area Primary Functions Quality Value
PLC And HMI Systems Line coordination, recipes, alarms, emergency stops, and process monitoring Stable operation and repeatable settings
Fiber Handling Control Fiber path alignment, payout management, and tension control Reduced risk of attenuation, microbending, and fiber breaks
Optical Performance Testing Attenuation, continuity, transmission, and fiber identification checks Confirmed optical performance
Mechanical Testing Tensile, crush, aging, jacket, and dimensional inspections Greater durability and more consistent cable output
Standards Control IEC 60794, ITU-T G.652D, ITU-T G.657A1, and ITU-T G.657A2 references Defined design and compliance objectives

How To Select Efficient Fiber Optic Cable Production Machinery

Initiate the selection process by examining the cable portfolio, not merely the machine list. Determine the plant’s production scope, encompassing various cable types such as drop, indoor, outdoor, and others. This approach ensures that the FTTH cable equipment selection is precise, avoiding costly production capability gaps.

Production Capacity And Line Speed

Match production output to expected demand, treating line speed as one part of the overall assessment. Coating and extrusion units can achieve speeds up to 1,000 meters per minute. In contrast, sheathing lines operate at approximately 60–90 meters per minute. The overall line output is determined by the slowest process, changeover time, and reel handling efficiency.

Assess fiber count, core diameter, cable diameter, lay length, material flow, take-up reel size, and setup time. High-speed fiber cable production lines must maintain consistent tension across all speeds. Request test data specific to the cable designs intended for the plant.

Evaluation Point Reason It Matters What To Verify
Line Speed Sets daily output and process balance Rated speed, normal operating speed, and loaded speed
Fiber Handling Capacity Supports existing and future cable products Core count, fiber type, and supported diameter range
Product Changeover Time Affects small-batch production Tool replacement, recipe storage, and reel-changing procedures
Material Throughput Controls jacket and buffer consistency Resin flow, cooling requirements, and material waste

Materials, Product Range, And Upgradeability

Confirm that the optical fiber cable-making machinery supports both single-mode and multimode fibers. The system should accommodate various fiber types, including G.652D and G.657A1/A2. Verify compatibility with materials such as Hytrel, PVC, LSZH, PE, steel tape, and wire armor.

A modular cable production line may combine processes such as fiber coloring, OFC 40 secondary coating, and OFC 60 jacketing. Request customization based on product drawings, core count, target speed, sheath materials, and required standards.

Modular equipment allows for future expansions. Adding new buffering, stranding, or jacketing units can extend the life of existing equipment. This flexibility supports adapting to changing orders without replacing the entire fiber optic cable line.

Factory Space, Energy Consumption, And Maintenance

Review the factory before purchasing the equipment. Many systems require a 380 V AC ±10%, three-phase industrial supply. Power consumption may approach about 55 kW, depending on the configuration. Confirm the necessary floor space, material flow, reel movement, ventilation, cooling water, operator access, safety clearances, and expansion space.

Compare energy-efficient extrusion units and UV-curing systems with the products planned for manufacture. Review preventive maintenance tasks, cleaning needs, spare-parts access, and service clearance around each module. Clear records and easy access are essential for maintaining the productivity of optical fiber cable-making machines during extended production periods.

A well-planned purchase integrates capacity, materials, layout, energy use, and service support. These considerations form a solid foundation for reliable FTTH production, avoiding unnecessary expenses on unused speed or features.

Installation, Training, And Support For FTTH Cable Manufacturing

The foundation of dependable FTTH cable line installation lies in a meticulously crafted factory plan. Suppliers must meticulously assess the floor area, production flow, access routes, and safety zones prior to equipment delivery. This foundational plan dictates the precise positioning of equipment, ensuring seamless coordination with utilities, line assembly, and cable routing.

Commissioning includes essential steps such as power checks, air and water connections, control-system setup, and process calibration. Engineers are dispatched upon equipment arrival, aligning with the equipment’s complexity, site readiness, and customer needs. Initial production verification is imperative to validate output quality before transitioning to regular operations.

Selecting a turnkey cable production system involves more than receiving machinery. It includes layout design, installation support, operator training, and detailed technical documentation. These documents are indispensable, detailing machine settings, wiring diagrams, operational procedures, maintenance tasks, and safety protocols. Such documentation is instrumental in minimizing downtime and ensuring efficient production management.

Good training for fiber optic cable machinery should combine technical instruction with hands-on practice. Operators must be proficient in handling fibers, loading materials, setting recipes, adjusting tension, and conducting extrusion, stranding, and cable testing. Training should also encompass routine cleaning, safe operation, alarm monitoring, and basic troubleshooting techniques.

Training may combine on-site practical sessions with remote reviews of control screens, recipes, and standard operating procedures. This dual approach ensures that operators are well-prepared to handle the complexities of the equipment.

  • Check fiber routing, tension control, and material-feed settings.
  • Check extrusion temperature, line speed, cooling, and jacket dimensions.
  • Inspect stranding settings, test results, and production records.
  • Practice safe shutdown, cleaning, inspection, and fault recovery.

Remote technical support can assist with software settings, program faults, sensor alarms, and equipment problems. A dedicated service team can review operational data, guide diagnostic procedures, and provide replacement support when necessary. Timely response is critical, given the operational demands of a production line serving active customer orders.

Preventive maintenance is essential, encompassing cleaning, lubrication, electrical inspections, calibration checks, and wear-part reviews. Modular equipment typically follows a maintenance cycle of approximately six months. The actual interval, influenced by operating hours, materials, dust levels, line speed, and site conditions, should be clearly outlined in a service plan.

Support Area Details To Confirm Before Purchase
Technical Support Response Support hours, response targets, escalation steps, and communication channels
Spare Parts Stock location, delivery time, compatible parts, and replacement procedures
Software Support Program backups, updates, access rights, and remote diagnostic options
Warranty Warranty period, exclusions, labor terms, and claims procedure
Local Service Regional engineers, travel assistance, and available maintenance coverage

Made-in-China.com Secured Trading and similar services may provide payment protection, shipment tracking, optional pre-shipment inspections, and dispute assistance. It is imperative to confirm details such as freight costs, delivery dates, warranty coverage, and service conditions directly with the chosen supplier.

Advantages Of Modern FTTH Cable Manufacturing Technology

Modern production systems give manufacturers precise control from fiber pay-off through to final jacketing. The integration of automated tension control, synchronized drives, stable extrusion, controlled curing, and precise stranding ensures the maintenance of cable dimensions and optical performance. This level of precision is critical for the production of advanced FTTH cables, catering to the demands of complex network projects.

Consistent Cable Quality And Lower Production Waste

Accurate process control is instrumental in maintaining a stable excess fiber length throughout the cable production process. This control supports controlled post-shrinkage, accurate lay length, precise binding, and repeatable jacket dimensions. Such factors are essential in reducing stress on the fiber, ultimately protecting signal quality during both installation and service.

Stable line control can reduce fiber breaks, material waste, and rework. It allows for more predictable output across extended production runs. The adoption of energy-saving extrusion systems and UV-curing technology further contributes to lowering operational costs, aligning with the goal of low-waste cable production.

Flexible Manufacturing For Changing Market Demand

A suitably configured line can manufacture indoor, outdoor, FTTH, armored, ribbon, loose-tube, and tight-buffered cables. The same equipment platform can also support datacom, hybrid, and composite designs with the addition of specific process modules. This adaptability enables manufacturers to respond to shifts in local broadband, data center, and enterprise network demands.

Individual process steps can be installed incrementally, allowing for expansion as orders increase. Modular equipment supports various functionalities, including rollable ribbon, fiber bundling, SZ super-bundling, and final jacketing. These capabilities cater to both high-density data center interconnect cables and standard FTTH products.

Modular upgrades can update older production lines without replacing every machine. New controls, drives, tension systems, and testing units can extend the service life of equipment and enhance productivity. This strategy safeguards existing investments while pursuing the latest advancements in fiber cable manufacturing technology.

Scalable Solutions For High-Speed Fiber Cable Production

Industrial lines designed for long batches and continuous operation can significantly increase output while maintaining process stability. Automated line synchronization ensures that pay-off, stranding, extrusion, curing, and take-up units operate at a consistent pace. These features are essential for high-speed fiber cable production, facilitating large-scale network deployments.

Effective FTTH cable production solutions involve more than high-speed machinery. They encompass operator training, global installation support, process guidance, and lifetime technical assistance from the supplier. Skilled teams can promptly identify process changes, ensuring reliable production over time.

Scalable machinery helps manufacturers match production capacity and cable quality with future network demand. This alignment provides a practical framework for growth across residential broadband, enterprise systems, and high-density fiber infrastructure.

Conclusion

A modern FTTH Cable Production Line integrates fiber preparation, coloring, secondary coating, buffering, stranding, extrusion, sheathing, testing, and automation into a unified workflow. Each phase ensures stable optical performance, precise dimensions, and reliable cable protection.

Choosing the right setup depends on cable design, fiber count, materials, standards, production volume, factory space, and planned expansion. Essential components include a fiber coloring machine, a fiber secondary coating line, a tight buffering line, an SZ stranding line, an advanced FTTH cable extrusion line, a fiber cable sheathing line, a fiber ribbon line, and compact fiber unit solutions.

Manufacturers must focus on maintaining controlled fiber tension, utilizing reliable materials, implementing automated monitoring, and conducting thorough quality tests. Optimal FTTH cable production solutions might encompass single process modules or complete turnkey systems, catering to various cable types such as indoor, outdoor, FTTH, armored, ribbon, and high-density datacom cables.

Using suitable fiber optic cable manufacturing equipment can improve production output while reducing waste. Scalable, upgradeable systems are instrumental in ensuring reliable broadband deployment, fortifying FTTH network manufacturing, and fostering long-term competitiveness.

Related: Ribbon Cohesion on a Fiber Ribbon Line
         Quality-Control Checklist for Every Fiber Draw Tower Pull

Precision Machining Services Houston – Expert CNC Solutions for Every Industry

Houston’s manufacturing sector attracts procurement managers and design engineers who require accurately produced components. Texas manufacturing contributes nearly 12% of the state’s total economic output, generating approximately $226 billion while supporting almost 900,000 jobs. Such a large manufacturing base allows Houston industrial machining services to expand their expertise, capacity, and range of available solutions.


This guide examines the Houston machining market, covering nearby machine shops, national precision firms operating locally, and contract manufacturers serving the wider region. Featured businesses include Lowrance Machine at www.lowrancemachine.com, RBR Machine, and contract manufacturers such as Centerline. Collectively, they reveal the depth and range of capabilities available throughout the Houston machining sector.

This guide is intended to help product developers, purchasing teams, and OEMs in oil and gas, aerospace, medical-device, industrial, and related markets identify the most appropriate machining company in Houston. The discussion includes conventional CNC milling, complex five-axis operations, precision component production, and fully managed turnkey services. Later sections explain available technologies, production capabilities, and supplier-selection criteria so teams can compare providers by tolerance control, turnaround time, and additional value-added services.

Main Points To Remember

  • Houston’s large manufacturing economy makes the region a dependable source of precision-machining services.
  • The featured suppliers include local specialists, including Lowrance Machine, together with nationwide manufacturers operating in Houston.
  • Available capabilities extend from straightforward CNC milling to sophisticated five-axis machining and complete turnkey manufacturing.
  • The primary audience includes procurement managers, engineers, product developers, and OEM decision-makers.
  • Later sections examine selection criteria, project costs, lead times, and practical use cases for choosing a Houston machine shop.

Houston Industrial Machining Services: Market Overview And Industry Context

Manufacturing activity throughout Houston has grown substantially in response to rising requirements from energy, aviation, healthcare, and petrochemical businesses. Demand for sophisticated, high-accuracy components has fuelled investment and expansion among Houston-area machine shops. Houston’s location near major highways, shipping ports, and railway networks also helps lower transportation expenses and shorten delivery schedules for regional customers.

Texas has a substantial population of experienced machinists and engineers capable of producing advanced parts on three-axis, four-axis, and five-axis machining centres. This expertise enables more parts to be completed in one setup, decreasing cycle duration and making Texas industrial machine shops more productive. The regional skills base makes it easier for shops to adopt updated technologies and production methods without extended staffing searches.

Advanced equipment is a standard feature of daily production within many Houston machining facilities. Five-axis CNC machines reduce fixture requirements and minimise changeovers when producing parts with intricate shapes. Wire EDM systems create detailed features in hardened metals, delicate sections, and thin components. Large-format milling machines allow regional manufacturers to complete oversized, single-piece work that might otherwise be sent to facilities outside Texas.

Quality-assurance equipment is just as important as machining equipment when producing critical components. Many shops use Zeiss coordinate measuring machines for first-piece reports, production inspection, and ongoing dimensional confirmation. These technologies verify that important components meet demanding specifications while delivering repeatable, documented, and traceable results.

A Houston-based machine shop allows customers to communicate directly and attend engineering or first-article sessions without extensive travel. Being geographically close enables quicker responses when demand shifts, designs change, or emergency orders arise. These benefits reduce offshore supply risks and provide both direct local assistance and the marketability associated with made-in-USA production.

CNC Machine Shop HoustonCNC Machine Shop Houston

Notable Machining Companies And Their Competitive Strengths

The Houston machining industry consists of independent local shops together with specialised contract-production businesses serving broader markets. Together, these providers offer shorter schedules, more hands-on cooperation, and clearer transportation arrangements than remote vendors. The providers below demonstrate strong CNC capabilities as well as wider industrial-manufacturing services.

Lowrance Machine is recognised in Houston for responsive customer service and close working relationships. The business focuses on CNC milling, made-to-order machining, and fabrication while prioritising quick project completion. The nearby facility supports direct quality checks, convenient meetings, and flexible supply-chain management for clients seeking an agile Houston machine shop.

RBR Machine specialises in high-accuracy production, multi-axis machining, and associated manufacturing support. Its certifications and registrations include ISO 9001:2015, ISO 13485, AS9100D, and ITAR, while its services extend from prototyping to finished assembly. The provider supports demanding sectors through quick quotations, detailed CMM measurement, API threading services, strong quality systems, and accelerated scheduling options.

Centerline and similar regional contract manufacturers provide adaptable production solutions for low-, medium-, and high-volume requirements. Centerline operates as a Houston contract manufacturer holding ISO 9001:2015 and AS9100D certifications. These nearby manufacturers strengthen sourcing flexibility, shorten response times, and offer many buyers a reliable substitute for overseas suppliers.

Choosing between these companies requires consideration of design difficulty, compliance requirements, production volume, and turnaround needs. Work requiring complex 5-axis capability or large machining envelopes often fits providers with resources similar to those of RBR Machine. Jobs requiring frequent communication and rapid local turnaround may be better served by Lowrance Machine or another nearby Houston shop with highly responsive customer support.

Featured Company Primary Capability Key Certifications Most Suitable Projects
Lowrance Machine Houston-based milling, fabrication, and rapid customer assistance Established manufacturing procedures and in-house quality checks Made-to-order work requiring local communication and rapid completion
RBR Machine Five-axis machining, large-format milling, and turnkey production ISO 9001:2015, ISO 13485, AS9100D, and ITAR Tightly toleranced work requiring advanced equipment and documented compliance
Centerline Houston Flexible contract production from limited quantities to high volume ISO 9001:2015 and AS9100D Certified domestic production runs and scalable sourcing requirements

When selecting CNC machining Houston partners, compare lead times, certification status, inspection resources, pricing, and geographic proximity. Houston-area companies bring together skilled production, responsive service, and supporting manufacturing capabilities for customers in multiple industries.

Important CNC Machine Shop Capabilities And Supporting Services

Selecting an appropriate CNC provider involves carefully assessing technical capability, inspection controls, available machinery, and production support. Buyers should verify that the company maintains disciplined quality-control practices and modern equipment while offering services that simplify the wider supply chain. Shops offering precision machining together with fabrication and downstream operations reduce handoffs by delivering parts prepared for the next production stage.

High-accuracy machining requires disciplined management of tolerances throughout production. Depending on the material, design, and intended application, common tolerance bands often fall between ±0.001″ and ±0.005″. Aerospace, healthcare, and defence manufacturers often rely on CMM reports, first-article inspection, optical systems, nondestructive examination, and hardness tests. Certifications such as ISO 9001:2015, AS9100D, and ISO 13485 demonstrate documented workflows that support audits, traceability, and customer acceptance.

For highly toleranced components, independent CMM inspection services can confirm dimensions even when another supplier manufactures the parts. The option improves dimensional validation while allowing the original manufacturer to remain in place.

Modern machining resources allow complicated components to be produced more efficiently and with fewer operations. Five-axis machining in Houston reduces repositioning and setup counts while creating contoured parts used in aerospace, medical, and other precision applications. Wire EDM allows suppliers to cut fine slots, sharp profiles, and complex details in metals that conduct electricity. Large-format milling handles oversized energy and heavy-equipment components using machine beds that may exceed 100 inches in length and width.

Additional machining processes allow more complex part families to remain with one supplier. Small precision parts suit Swiss-style turning, whereas robust CNC turning centres handle greater diameters and extended lengths. A provider combining CNC milling in Houston with specialised turning and wire EDM can complete complicated groups of related components under one roof.

End-to-end manufacturing simplifies purchasing, lowers administrative effort, and helps accelerate delivery. An effective turnkey provider may coordinate everything from early design and prototypes to machining, finishing, assembly, and shipment. Regional contract manufacturers frequently bundle plating, anodising, heat treatment, kitting, and supply-chain management within one purchase order.

For urgent programs, supporting operations can determine whether delivery targets are achieved. Expedited scheduling, internal finishing, and in-house assembly reduce supplier handoffs and shorten time-to-market. Choosing a provider that combines turnkey manufacturing with metal fabrication and machining creates clearer accountability and better control of finished-part quality.

How To Evaluate And Select A Machining Partner In Houston

Begin by defining the project requirements in clear and measurable terms. Document anticipated part volumes, specify whether the work is developmental or production-based, and list every required material. Include tolerance ranges, finish requirements, and any aerospace, medical, defence, or other compliance obligations. This level of clarity improves quoting accuracy and lowers the likelihood of late engineering changes or pricing disputes.

Before placing an order, confirm that the supplier’s certifications and quality-management procedures match the project’s requirements. Ask whether the business holds ISO 9001:2015, AS9100D, or ISO 13485 certification and whether ITAR registration is maintained for defence programs. These standards support traceability, process documentation, inspection control, and regulatory acceptance within precision-machining services.

Evaluate whether the provider’s equipment and technical knowledge match the part’s actual manufacturing requirements. Where needed, ensure the shop operates multi-axis centres, EDM equipment, precision turning machines, and large-bed mills. Also review CMM inspection capacity and secondary services such as heat treatment, plating, coating, fabrication, or assembly. Reliable Houston machining companies normally publish or provide machine lists, capacity details, and examples of similar completed work.

Compare quotation response times and realistic production lead times before choosing a supplier. Vendors capable of supplying prompt, transparent quotations and genuine rush options may reduce project risk. Fast quoting and clearly stated timelines improve project planning and help control supply-chain uncertainty.

Review how each shop measures parts, records results, and reports quality information to customers. Obtain examples of coordinate-measurement reports, FAI documents, material certifications, and completed inspection data. Reliable providers maintain detailed records that demonstrate conformity and simplify acceptance by customers or regulators.

Communication quality and access to local support should be treated as important supplier-selection factors. Face-to-face design reviews, factory visits, and geographic proximity reduce logistics costs and accelerate problem resolution. A regional supplier often offers better supply-chain adaptability and quicker support for unexpected requirements.

Compare the complete landed cost of Houston machining with the true expense of purchasing from offshore suppliers. Include shipping, duties, warehousing, delays, rejected parts, communication overhead, and revision costs in the calculation. Once hidden costs and market-launch timing are considered, custom machining from nearby shops may prove more economical than overseas alternatives.

Examine references, case studies, and the supplier’s history within relevant industries. Look for proven performance in oil and gas, aerospace, medical, automotive, power generation, or other applicable sectors. The strongest evidence includes relevant finished parts, quality outcomes, and consistent schedule performance.

Determine whether the supplier can support the project after initial delivery and expand production when demand grows. Evaluate whether the shop can support prototypes, pilot runs, regular production, final assembly, and longer-term sourcing agreements. A scalable precision-machining service reduces the need to transfer mature products to a different manufacturer later.

Supplier comparisons become more consistent when teams score technical specifications, quality credentials, machinery, quoting, documentation, support, cost, history, and production scalability. A methodical selection process helps identify a provider capable of meeting technical demands as well as purchasing and business expectations.

Houston Industrial Machining Costs, Delivery Times, And Practical Applications

Several variables influence Houston machining rates, including geometry, raw material, setup requirements, and batch quantity. Costs also rise when parts require extremely close tolerances, specialised inspection, thermal processing, or surface finishing. Complex shapes and difficult materials such as titanium typically raise machine time and hourly cost. Although 5-axis machining may involve higher programming and initial setup charges, it can lower the total project cost by eliminating multiple setups and fixtures.

A realistic project budget includes more than the cost assigned to each machined component. Additional costs may include communication time, freight, tariffs, inventory, quality problems, and schedule delays. Houston-area suppliers may lower indirect costs by simplifying logistics and allowing faster communication than offshore manufacturers.

Lead times for Houston machining depend on supplier workload, part difficulty, material availability, and the overall project scope. Providers that respond quickly and reserve accelerated machine time help customers move from design to finished parts sooner. Nearby machining reduces transportation complexity and allows projects to progress without the extended shipping associated with overseas suppliers. Being close to the supplier makes it easier to implement drawing changes, replace rejected parts, and respond to sudden demand.

A regulated manufacturing program benefits from suppliers that can demonstrate certification, traceability, controlled processes, and accurate CMM measurement. Strong compliance and measurement systems minimise rejected components, corrective work, approval problems, and production delays.

Practical industrial applications demonstrate the range and value of Houston machining capabilities. Energy-sector work may involve oversized mills, rugged materials, API-related features, and components built for severe operating conditions. Complex flight and defence parts generally require 5-axis capability, AS9100D systems, controlled records, and exact dimensional verification. Medical projects often use wire EDM and Swiss machining alongside ISO 13485 systems and comprehensive traceability. Large mills, resilient alloys, and protective surface treatments support many power-generation and renewable-energy applications.

Providers that offer quick prototypes and end-to-end production support can move projects forward with fewer delays. The same provider may support initial samples, design refinement, production launch, finishing, and assembly with limited outsourcing.

For time-sensitive or compliance-intensive projects, prioritise local providers that demonstrate rigorous process control and dependable coordinate measurement. Choose providers with documented multi-axis experience when designs involve compound angles, deep features, or complex surfaces. Contract-production companies can be advantageous when quantities vary or when ongoing manufacturing capacity is required. A sourcing strategy that uses a responsive local shop like Lowrance Machine together with specialist regional capabilities can optimise price, lead time, and engineering performance.

Related: The Surface Finish Achieved With Injection Molds in Houston

Custom Mold Building Services Dallas

Lowrance Machine is a trusted provider of precision manufacturing and industrial mold support at
www.lowrancemachine.com
. We serve the greater DFW region with dependable, purpose-built production for a wide range of industries.

The Lowrance Machine team applies advanced CNC machining techniques to provide consistent accuracy and fast turnarounds. We combine experienced staff, modern equipment, and strict quality checks to achieve tight tolerances.


Customers using our Dallas services gain from many years of practical shop experience in Dallas CNC operations. Whether your business is a small startup or a major production operation, our CNC shop is set up to produce specialized parts and complicated machining jobs.

Ask for a production-ready estimate today to review your project needs. Lowrance Machine can streamline your manufacturing process and deliver the responsiveness your business requires.

Dallas CNC Lathe Machining Services For Professional Results

Lowrance Machine combines four decades of shop experience with strict engineering checks to deliver dependable, precision parts. The goal is straightforward: produce accurate parts with reliable manufacturing support for Dallas-area manufacturers.

Precision Engineering Standards

With decades of machining knowledge, our manufacturing facility follows strict inspection procedures. We use documented processes to hold close tolerances and check every run for repeatable accuracy.

Serving The Dallas Metroplex

Lowrance Machine works throughout the full Dallas Metroplex with flexible production and quick turnaround. The shop provides CNC milling, CNC turning, and related machining support to handle difficult engineering requirements.

  • Complete precision machining support for prototype and production parts.
  • Dedication to close tolerances and consistent quality.
  • Local production support and responsive service for area manufacturers.

Why Manufacturers Choose Lowrance Machine For Custom Projects

Our Lowrance Machine shop supports the move from engineering designs into consistent production results with a realistic, hands-on manufacturing method. Our facility brings together decades of manufacturing know-how with strong engineering understanding to handle difficult requirements.

Customers appreciate our experienced team for responsive updates and careful project coordination. We work closely with customers to verify specifications and prevent avoidable rework, so components leave on schedule and to specification.

Transfer Molds Dallas

Quality sits at the center of every process. Our team applies recorded inspection steps to protect dimensional consistency across production and to ensure finished parts match your design intent.

  • Experienced machinists who convert design intent into production-ready parts.
  • Clear schedules and timely project updates throughout your manufacturing process.
  • Dependable results that support lower costs and faster production for industrial customers.

Advanced CNC Turning, Milling, And Machining Capabilities

Our facility relies on advanced 11-axis equipment to machine difficult geometries while holding close tolerances. This advanced axis capability broadens the machining possibilities for complex components and shortens setup time for repeat work.

Advanced Multi-Axis Machining

Coordinated multi-axis machining lets us access challenging areas of a part in one setup. Less part repositioning help improve consistency while limiting alignment problems.

This machining capability helps produce complex designs and a broad mix of metals and engineered materials.

High-Speed CNC Milling

High-speed machining supports smooth surfaces and efficient machining cycles. We pair spindle speed with optimized toolpaths to maintain accuracy while meeting required specs.

Turning Operations

The shop’s CNC turning work emphasizes dimensional accuracy and finish quality. Every component is checked to verify dimensions and surface finish.

  • 11-axis equipment for intricate, repeatable results.
  • Fast milling and precision CNC milling for demanding dimensional specifications.
  • Inspection integrated into production to ensure manufacturing standards.

Precision Machining For Many Industrial Sectors

Our facility supports industries from energy to aerospace with repeatable, high-quality production.

The shop delivers close-tolerance machining services for many industrial sectors, including large regional companies and Fortune 500 businesses based in the area.

Our production strengths serve high-demand markets such as aerospace, energy, and defense where reliable machined parts are essential for safety and uptime.

Through advanced CNC milling and turning equipment, we provide dependable production outcomes that meet strict specifications.

  • Precision production for prototypes and long runs to help production timelines stay on track.
  • Quality checks that ensure each part conforms to customer requirements.
  • Flexible services to handle unique part geometry and material needs.

We serve a wide range of sectors with the manufacturing knowledge needed to remain competitive. Every machined part is manufactured to meet both performance and quality goals.

Commitment To Tight Tolerances And Quality Control

The shop reinforces accuracy with quality systems and continuous process checks. The operation maintains ISO 9000-compliant quality practices and use Statistical Process Control to keep variation low and accuracy high.

Statistical Process Control Methods

SPC monitoring helps keep processes stable and components inside specification. Current control charts and documented plans show variation trends so problems can be corrected before bad parts are produced.

We prioritize precision machining standards so finished components match the specified tolerance range. Modern inspection tools verify dimensions and surface finish at important production checkpoints.

  • ISO 9000 quality systems that document process steps and audits.
  • SPC methods that help control variation while improving production flow.
  • Measurement routines that validate accuracy across runs.

Through the combination of SPC and process discipline with experienced staff and calibrated equipment, we minimize waste and deliver consistent, high-quality parts for your industrial projects.

Modern Equipment And Technology Advancements

A climate-controlled 43,000 sq. ft. facility in Fort Worth supports the space and control to run sensitive projects with stable results.

Our machine shop houses the latest equipment to handle high-accuracy machining and complicated components. Ongoing equipment upgrades keep our production lines current and efficient.

Our shop functions as an advanced CNC machine shop by investing in tools that improve throughput and lower variation. That investment supports more reliable accuracy and improved quality across each project.

Modern technology also strengthens workflow. Real-time monitoring, advanced controls, and automated toolpath strategies allow the team to hold accuracy and protect project schedules.

Equipment Category Key Capability Production Use Practical Advantage
Multi-axis machining centers Difficult geometry Complex production components Less handling with better repeatability
High-speed milling centers High-quality machined finish Short runs and long production runs Improved production speed
Automatic inspection systems Real-time verification In-process checks Lower scrap, higher quality
Tool management systems Efficient tool planning Repeat runs Less downtime

Efficient Lead Times And Streamlined Production

We compress schedules without cutting corners so parts move from design to delivery faster.

Our production schedule runs twenty hours daily during the workweek. This extended schedule helps reduce lead times while maintaining careful quality control.

Rapid Prototyping

Quick prototype production moves concepts into physical parts quickly. Our engineers and operators work together to improve the design and confirm function in the first stages of production.

Fast-turn prototypes allow customers to review designs sooner and make informed choices quickly.

Scalable Production Runs

We scale from single prototypes to full production runs without changing the core process. The stable process protects accuracy and helps keep costs predictable.

  • 20-hour daily operations support quicker ramp-up and improved delivery timing.
  • Controlled processes protect consistent quality for both small batches and long production runs.
  • Efficient workflow supports reliable CNC machining and on-time production for manufacturing partners.

Secondary Machining And Custom Finishing Options

We apply tailored finishing and secondary processes to help every part satisfy appearance and performance requirements. Lowrance Machine supports thermal processing, plating, and coating services matched to your material requirements and final application.

We integrate these secondary steps into production so finished machined parts are ready for the next stage. The result is less handling and a faster move toward final use.

Common finishing services include hardening, anodizing, passivation, and protective coatings. The shop can also deliver precise surface finishing for improved appearance and functional wear life.

  • Heat treat and hardness control for extended durability.
  • Plating and coatings tailored to material and environmental needs.
  • Final machining, deburring, and inspection built into production.
Finishing Service Main Purpose Benefit Often Used Materials
Heat treatment Raise material strength Improved wear resistance Steel and alloy materials
Metal plating Protection from corrosion Extended service life Brass and steel
Coatings & finishing Surface function and visual quality Consistent quality and fit Composites and aluminum

By controlling the complete path from precision machining through final treatment, we satisfy detailed requirements and provide dependable high-quality parts, whether your requirement is appearance-based, performance-based, or both.

Logistics And Inventory Management Support

Our team matches delivery schedules to your production flow so parts arrive exactly when needed. That planning process minimizes stored inventory without interrupting production.

The Lowrance Machine team provides practical logistics services, including just-in-time delivery and flexible warehousing. Our machine shop coordinates steady schedules with clients to reduce lead times and improve supply flow.

Just-In-Time Delivery And Support

We coordinate shipments, track orders, and adjust runs to match changing customer demand. That lowers inventory levels and reduces carrying costs.

Our planning integrates seamlessly with your production process. This helps ensure reliable delivery of high-quality machined parts on the agreed timeline.

Support Service Customer Advantage Common Use
JIT delivery Reduced inventory and less waste Regular part restocking on daily or weekly schedules
Adaptable warehousing Buffer stock, rapid dispatch Short-term or long-term storage
Production schedule coordination More predictable lead times Coordinated manufacturing planning

Experienced Manufacturing Team And Expertise

Skilled machinists, technicians, and process engineers work together to convert designs into consistent, high-quality components. The team contributes long-standing industrial manufacturing knowledge to every production run and keeps quality consistent across many industries.

The shop blends experienced people with modern equipment to handle difficult production runs. The mix of experience and technology supports tight tolerances and stable production for repeat customers.

Our capabilities span initial design consultation, fixture development, setup, and final inspection. That complete-service method makes handoffs easier and helps reduce rework for customers.

  • Experienced staff who solve technical challenges and optimize process flow.
  • Modern equipment that handles varied materials and close specifications.
  • End-to-end services that keep production on schedule and within tolerance.

As an experienced Dallas CNC provider, we focus on strong service, accuracy, and quality. The facility remains prepared to support diverse component requirements and produce the accuracy your project needs.

Request A Quote For Your Custom Parts

Request quick pricing for your custom parts and production needs — our quoting team delivers same-day quotes for most requests. Tell us about your part design, material choice, and quantity so we can prepare accurate pricing as soon as possible.

Our team quotes CNC turning, CNC milling, and related machining services. Sharing accurate project details allows us to match the right capabilities and return competitive pricing quickly.

  • Fast quote turnaround for prototypes and production quantities.
  • Review design specifications, tolerances, and materials with a knowledgeable team.
  • Quick responses when drawings, quantities, and timelines are provided.

If you need a small prototype run or a high-volume part order, reach out to start the conversation. We aim to make quoting easy so your job continues moving.

Summary

When accuracy matters, our team works to deliver consistent results that keeps difficult manufacturing timelines moving.

Lowrance Machine continues to prioritize high quality and precision in every service. We deliver CNC machining and precision machining solutions that satisfy demanding tolerances while maintaining precision from prototype to full production.

Our organized workflows and reliable delivery schedules support many industries in reducing downtime and remaining competitive. Choosing our machining services means working with a provider that values efficient production, clear updates, and on-time results.

Get in touch today to review how our services can help your next project and support accurate parts delivered within the planned timeline.

Related: More Information About Machine Shop Dallas Delivering Custom Fabrication Services

CNC Lathe Machining Dallas Businesses Rely On For Accuracy

Precision cast inserts, though compact, play a pivotal role in supporting robust threaded connections within plastic, metal, and composite products. Lowrance Machine specializes in combining tooling, casting, and accurate CNC machining. This coordinated process enables the production of high precision cast inserts and machining in Dallas, catering to both limited production runs and high-volume production.

Industrial Machining And Repair Services In Dallas
Services offered by local cast inserts Dallas providers can greatly lower lead times and tighten logistics for manufacturers across a wide range of fields. Lowrance Machine uses modern techniques like rubber molds Dallas, compression molds Dallas, urethane casting, and die casting. These processes are comparable with those used by industry leaders such as Aluminum Die Casting Company and DyCast Specialties, helping deliver repeatable quality.

Yardley Inserts, with its long background in supplying both regular and specialized threaded metal inserts, highlights the market’s demand for both stocked and bespoke options. Lowrance Machine supports cast inserts manufacturing services in Dallas Tx, combined with post-cast CNC lathe machining services in Dallas. This full-service workflow delivers finished parts that align with demanding tolerances and assembly standards.

A Practical Overview Of Cast Inserts Manufacturing Services

Cast-in threaded inserts are precisely formed metal components embedded within a receiving component. They act as strong fastening points, supporting durability and resistance to wear. This manufacturing technique is well suited for applications requiring reliable connections in materials such as soft or engineered host materials.

Understanding Cast Inserts And Their Materials

Typical material choices for cast inserts include brass, steel, 304 stainless steel, and 316 stainless steel. Aluminum die casting often uses harder alloys to strengthen thread strength. Engineered plastics are used as supportive host materials, seamlessly integrating with polymer components.

Manufacturers such as Aluminum Die Casting Company and DyCast are recognized for combining die casting with precision machining. Yardley Inserts exemplifies the demand for both standard and custom cast inserts, meeting a large selection of production requirements.

Custom Cast Inserts In Dallas

Common Applications Across Industries

For furniture producers, cast inserts reinforce joints and mounting points, supporting the stability of hardware. Medical device manufacturers use them for housings and assemblies that necessitate precise tolerances and consistent fastening. The electronics sector incorporates inserts as PCB standoffs and heat-sink mounts, where both electrical and thermal performance are important.

Defense and marine hardware heavily use cast inserts for applications such as sealed tube assemblies, mounting brackets, and corrosion-resistant fittings. These environments call for materials and processes capable of handling stress and exposure.

How Lowrance Machine Supports Cast Insert Production

Lowrance Machine offers full-service cast inserts manufacturing services, encompassing mold building, casting, CNC finishing, and assembly integration. By pairing die casting with precision machining, the company supplies inserts ready for immediate installation, helping contract manufacturers.

As a capable machine shop in Dallas for custom metal parts, Lowrance Machine caters to local OEMs requiring timely production. For businesses seeking a precision machine shop in Dallas for industrial components, the company streamlines the process from tooling to quality checks, promoting uninterrupted production.

Service Capability Usual Materials Common Use
Tooling and mold building Steel cores and aluminum tooling Development parts, small batches, and production molds
Die casting and sand casting Aluminum alloys, brass, zinc Volume insert production for furniture and electronics
Post-cast CNC machining and finishing Stainless grades 304/316 and hardened steel Critical parts for medical, marine, and military uses
Integration, kitting, and assembly preparation Specified housing and insert material combinations Consumer products and electronics assemblies

Benefits Of Cast Inserts For Precision Components

Cast inserts emerge as a practical solution for designers aiming to incorporate metal threads within softer materials. They facilitate the creation of a robust metal-to-metal interface, thereby increasing thread durability and performance under wear and tear. This is critical in environments where repeated assembly cycles are inevitable, as it can sharply decrease the risk of thread stripping in plastics and composites.

Integrating cast inserts often reduces the necessity for extra hardware or adhesives, thereby streamlining the assembly process and lowering long-term expenses. In many applications, these inserts improve upon the performance of press-fit fasteners and direct tapping in plastic, supporting extended service lifetimes and a lower frequency of field repairs.

For development batches and limited runs, urethane or silicone casting offers a quick and affordable alternative to injection molding. The creation of silicone molds can be expedited to a timeframe of one to two weeks, whereas aluminum tooling may require a month or more for preparation. This disparity demonstrates the efficiency of these casting methods in speeding the development cycle.

Urethane casting frequently delivers comparative advantages over repeated 3D printing for larger prototype batches. It enables a reduction in per-piece costs and an enhancement in surface finishes, thereby improving the validation of design iterations prior to the investment in production tooling.

Working with local manufacturing entities in Dallas can greatly shorten lead times and limit shipping-related delays. A Dallas CNC machine shop, adept in short run and production machining, can speed up the transformation of prototypes into finished parts. For those requiring extra finishing, CNC lathe machining Dallas businesses are renowned for their precision and consistency in achieving tight tolerances.

Working alongside a dependable CNC machining company serving Dallas manufacturers promotes the project’s timely completion. Local mold builders and precision shops provide rapid tooling, finishing, and quality assurance services. This local coordination supports both singular prototype creations and repetitive production cycles, eliminating the need for lengthy delays.

Cast Inserts Manufacturing Services In Dallas Tx

Dallas-area shops bring together mold making, casting, and finishing under one roof, increasing production efficiency. They support silicone mold building for prototypes and compression tooling for short runs. This approach supports rapid iteration and ensures superior final part quality.

Dallas Capabilities For Mold Building, Casting, And Finishing

Dallas-area manufacturers support mold building services for manufacturing operations. They are skilled at creating both rubber molds and precision compression molds. Silicone molds are completed within one to two weeks, making urethane casting well suited for functional prototypes. For metal inserts, die casting or gravity casting is integrated with CNC turning and milling to meet precise tolerances.

Benefits Of Working With A Dallas-Area Supplier Like Lowrance Machine

Lowrance Machine provides integrated workflows that bring together mold building, casting, and post-cast CNC lathe work. This process reduces handoffs, helping create consistent results. Customers receive 3–5 axis machining, CMM inspection, and surface treatments, all within the metro area.

Regional Sourcing Benefits For Dallas Manufacturers

Nearby supply can reduce transit time and shipping costs, supporting communication during design and tooling stages. This compresses the loop between engineering and the shop, improving problem-solving for tight schedules. For manufacturers requiring rapid prototypes or small production runs, local cast inserts manufacturing services in Dallas Tx deliver substantial logistical benefits.

Selecting Materials And Processes For High Precision Cast Inserts

The selection of metal and manufacturing process strongly affects the performance, cost, and delivery time of cast inserts. This guide gives an overview of typical options and the role of secondary operations in achieving precise specifications for complex assemblies.

Common Metal And Alloy Options

Die-cast aluminum alloys are commonly chosen for their lightweight properties and resistance to corrosion, making them useful for consumer and electronic components. Stainless steels, including 304 and 316, are preferred for their corrosion resistance in marine and medical applications. Hardened tool steels are well matched to high-wear, load-bearing roles in industrial machinery. Brass and bronze, known for their corrosion resistance and ease of machining, are frequently selected in decorative and electrical components.

Casting And Prototype Mold Options

Gravity casting, investment casting, and aluminum die casting are commonly used for metal inserts requiring mechanical strength. Urethane casting with silicone molds creates a rapid, cost-effective solution for prototypes and small batches. This method enables the validation of form and fit without the expense of aluminum or steel tooling. Suppliers in Dallas often deliver low-volume silicone mold options, speeding development timelines.

Secondary Machining And Finishing

Following the casting process, precision machining refines tolerances and improves surface quality. Common secondary operations include thread rolling, turning, milling, drilling, and slotting. Surface treatments such as plating or passivation can improve the lifespan of components in harsh environments. Local machine shops in Dallas operate advanced CNC lathe machining and multi-axis milling to satisfy stringent specifications, as outlined by industry leaders like DyCast and Lakeside Screw Products.

Selection Guide And Process Tradeoffs

Urethane casting can be economical for small runs, offering a balance of cost and speed. For larger production volumes, metal casting combined with secondary machining can reduce costs per unit and strengthen mechanical properties. Engineers must evaluate material properties, expected wear, and necessary post-casting operations to hold final specifications.

Custom Cast Insert Applications In Dallas

For Dallas custom cast insert projects, manufacturers can use both mold builders and precision shops. Combining resources for compression molds in Dallas with full metal casting and CNC lathe machining ensures a seamless transition from concept to production.

Tooling Options For Cast Insert Production

The selection of tooling significantly influences the cost, lead time, and quality of cast inserts. Local expertise supports rapid iteration and cuts down waste. An experienced mold builder in Dallas for custom tooling solutions provides practical design options. These options help prevent defects, support part release, and support tool longevity.

How Local Mold Makers Help

Partnering with skilled tooling partners in Dallas during design reviews is important. They propose draft angles, venting, and radii that enhance fill quality and lower porosity. These improvements reduce scrap and expedite production approval.

Compression And Silicone Tooling Options

Silicone molds remain practical for rapid, cost-effective urethane casting prototypes. They enable teams to validate form and fit within about 1–2 weeks. Conversely, compression molds are preferred for rubber parts, where controlled pressure is important for elastomer flow and cure. Shops offering rubber molds Dallas and compression molds Dallas provide short runs and functional prototypes without heavy upfront costs.

Choosing Between Metal And Elastomer Tooling

Metal tools made from aluminum or steel are often used in high-volume injection or die casting, supporting durability and consistency. These tools demand longer lead times and higher initial investments. However, they offer a lower per-part cost at scale and superior surface finish for machining and plating.

Balancing Lead Time And Cost

Tooling choices for prototypes favor speed. Silicone tools typically yield samples in one to two weeks. In contrast, aluminum or steel tooling may take four to eight weeks, based on complexity. The right choice depends on balancing run quantity, geometric complexity, and finish requirements.

Mold Building Services And Integration

Integrated mold building services in Dallas for production needs include master pattern making, tool trials, and maintenance plans. Working with local providers cuts shipping time and streamlines revisions during development. This facilitates a more predictable transition from prototype to production.

CNC Finishing And Post-Cast Operations

The process of refining cast inserts calls for meticulous machining and rigorous inspection. Dallas-based local shops use a combination of turning, milling, and measurement techniques. This approach transforms raw castings into components of exceptional accuracy. Such work ensures that parts hold stringent standards of diameter, concentricity, and thread quality, meeting the demands of aerospace, medical, and industrial sectors.

Accurate Lathe Finishing

Utilizing modern lathes, turning and single-point threading make possible the creation of parts with consistent thread form and concentric bores. These shops, experienced with CNC lathe machining services in Dallas, produce both prototype batches and volume production. Their ability to set up quickly and maintain consistent cycle times highlights their commitment to precision.

Complex Part Support Through Multi-Axis Milling

5-axis milling machines are important for handling parts with challenging geometries and multi-face features, reducing the need for multiple fixtures. Regional suppliers, equipped with such advanced machinery, support clients in Dallas who require parts with undercuts, compound angles, or simultaneous five-sided machining.

Quality Inspection And Surface Verification

Coordinate measurement equipment play a major role in validating critical dimensions and geometric tolerances. These machines, along with thread gauging, surface finish testing, and statistical sampling, guide quality assurance initiatives. Such measures are implemented to lower scrap and rework, raising overall efficiency and product quality.

Operation Core Capability Typical Application
Turning Accurate threading, controlled diameters, and 0.0005″ concentricity Internal and external threads on brass, bronze, and aluminum inserts
Five-axis milling Complex contours, multi-face indexing, single-setup precision Multi-feature inserts with angled faces and undercuts
CMM measurement 3D inspection, tolerance verification, and dimensional documentation Final acceptance for critical aerospace and medical components
Surface quality testing Surface roughness checks, polishing, and coating prep Cosmetic and functional finish verification for assemblies
Documented inspection plans Full or sampled inspection backed by documentation High-dependability production where every insert must conform

Working with a reputable CNC machine shop in Dallas coordinates the transition from casting to final machining. Such partnerships with CNC machining experts serving Dallas texas manufacturers help ensure that tooling selections and inspection protocols match the specific requirements of the end-use application.

Custom Fastener Support And Insert Integration

Combining cast inserts with matching fasteners supports assembly efficiency and extends part lifespan. Engineers in Dallas precisely coordinate insert geometry, thread forms, and material with fastener suppliers. This limits galling and sets installation torque. Local collaboration supports faster iteration, ensuring parts meet production goals.

Working With Matched Component Suppliers

Working with a custom fastener manufacturer in Dallas supports thread, size, and finish alignment with insert designs. Regional fastener shops and precision machine shops provide matched solutions for various fastener types. Yardley Inserts reflects the coexistence of standard and custom items in high-volume production.

Assembly And Reliability Design Considerations

Compatibility and expansion behavior are critical when specifying inserts and fasteners. Thread engagement length, installation method, and corrosion protection are important for long-term reliability. Assembly processes must set installation torque and retention methods, especially for vibration resistance.

Examples In Industrial Use

Custom cast insert applications in Dallas include electronics housings, furniture joints, medical device assemblies, and heavy marine fittings. Examples include stuffing tubes and heavy-duty ship components, demonstrating large-scale applications. Precision shops deliver secondary machining and matched fasteners, supporting parts are ready for assembly.

Assembly Application Insert Type Compatible Fastener Important Design Notes
Electronics enclosures Threaded brass insert M2–M4 machine screws Controlled torque, EMI concerns, and low thermal expansion
Furniture hardware assembly Die-cast zinc insert Hex fasteners and captive screws High retention strength, flush appearance, and finish plating
Medical components Stainless threaded insert Threaded studs and self-clinching fasteners Precise torque, corrosion resistance, and biocompatibility needs
Boat and ship hardware Bronze cast insert Threaded fittings and heavy-duty bolts Corrosion protection in saltwater, fatigue strength, and durability

Coordinating alongside a custom fastener manufacturer in Dallas and early specification of custom fasteners simplify design convergence. This method reduces rework and enhances retention under load. Local partnerships enable efficient testing and qualification for production programs.

Turnkey Cast Insert Services And Supplier Capabilities

One supplier handling each production stage streamlines schedules and supports part quality. Local manufacturers can progress from CAD models to finished hardware efficiently, removing the need to manage multiple vendors. This approach speeds the approval process, speeds up iteration cycles, and minimizes risks for projects with tight deadlines.

Start-To-Finish Manufacturing Services

Design support and prototyping form the foundation for dependable parts. Rapid 3D printing for masters and precision mold building prepare for urethane or die casting runs. CNC finishing and inspection confirm customers receive inserts ready for installation.

Lowrance Machine Capabilities

Lowrance Machine delivers mold building, casting, precision machining, and inspection under one roof. This combination supports a smooth transition from prototype to short-run production with consistent tolerances. Lowrance Machine coordinates with shop floor scheduling, coordinating volumes and delivery windows.

Finding The Right CNC Machining Partner

Collaborating with a trusted CNC machine shop in Dallas for custom machined parts minimizes handoffs and supports faster problem resolution. A reliable CNC machining company serving Dallas manufacturers delivers machining expertise, robust quality control, and rapid response to design updates.

Using turnkey cast insert services and local expertise significantly reduces lead times and helps keep projects within budget. Suppliers that bring together casting and machining capabilities create a single point of contact for engineering changes, inspection data, and delivery coordination.

Industrial Machine Repair And Maintenance For Production Stability

Maintaining production schedules for cast inserts depends on the efficiency of machine maintenance. Dallas-based localities support on-site technicians and comprehensive shop rebuilds. These services are designed to minimize downtime, supporting mold making, casting, and CNC finishing processes remain uninterrupted.

Why Rapid Service Helps Avoid Downtime

Unforeseen interruptions can significantly delay delivery schedules and drive up operational costs. The fast response of industrial machine repair specialists in Dallas is vital. It supports uninterrupted production shifts and reduces the accumulation of workloads. Furthermore, preventive maintenance agreements are instrumental in averting emergency situations by identifying potential issues before they become full-blown failures.

How Maintenance Supports Quality And Lead Times

Predictable lead times and consistent quality are directly connected to the regularity of maintenance activities. Tasks such as alignment, spindle tuning, and tool-offset checks are essential for maintaining dimensional precision in machined inserts. Additionally, the routine servicing of presses and grinding equipment is necessary to sustaining surface finish and tolerances, thereby supporting that production timelines remain consistent and scrap rates are minimized.

Manufacturer Repair And Field Service Options

Industrial service providers in Dallas offers a range of services, including machine tool rebuilding, field machining, on-site alignment, spindle repair, and parts support. These complete industrial equipment and machine repair services in Dallas, Texas, are intended to extend the lifespan of machinery and accelerate its return to operational status.

Selecting Service That Fits Production Needs

When selecting a service provider, it is imperative to evaluate response times, spare-parts availability, and the provider’s experience with similar equipment. Selecting a service that integrates industrial machine repair services in Dallas, Texas, with preventive maintenance programs is important. This service model helps ensure that manufacturers can meet their deadlines without compromising on the quality of their products.

Selecting A Dependable Cast Inserts Manufacturing Partner

The selection of a vendor should be based on their proven track record in cast insert production and their ability to swiftly transition from tooling to machining. Choose a partner that brings together mold creation, casting, and CNC finishing within a single facility. A precision machine shop in Dallas, recognized for industrial components, should provide documented quality assurance processes. These include CMM inspections, first-article reports, and traceable records, thereby lowering risk and accelerating the qualification phase.

Manufacturers should prioritize a vendor that delivers transparent cost and lead-time comparisons. This transparency is important when deciding between silicone or urethane tooling versus aluminum and steel. For smaller production runs, silicone tooling creates a cost-effective solution with a reduced lead time. Conversely, for larger volumes, aluminum or steel molds deliver superior durability and tighter tolerances.

Before making a commitment, request references, sample parts, and inspection reports. A trusted machine shop in Dallas, chosen by industry leaders, will share a detailed roadmap from prototype to production. They should also demonstrate their past collaborations with insert specialists, such as Yardley Inserts, to confirm their industry standing. Request specific details on turnaround times, anticipated scrap rates, and planned inspection protocols to clearly assess different vendors.

Think about the value of partnering with a local entity like Lowrance Machine, which provides seamless integration of mold building, casting, and precision machining. A local partner can help lower shipping times, allow easier on-site visits, and speed up the iteration process for Dallas manufacturers. Ultimately, select vendors with robust quality systems, comprehensive capabilities, and a transparent plan for tooling and volume to promote a smooth transition from prototype to production.

Related: Custom Mold Building Services Dallas

How an SZ Stranding Line Supports Better Cable Geometry and Stability

More than 60% of new broadband deployments in metropolitan U.S. projects now call for fiber-to-the-home. That accelerated move toward full-fiber networks highlights the immediate need for dependable production equipment.

Compact Fiber Unit
Fiber Secondary Coating Line
Fiber Ribbone Line

Shanghai Weiye Optic Fiber Communication Equipment Co (www.weiye-ofc.com) delivers automated FTTH cable production line systems for the United States market. Their turnkey FTTH Cable Production Line for High-Speed Fiber Optics integrates machines and control systems. It turns out drop cables, indoor/outdoor cables, and high-density units for telecom, data centers, and LANs.

This advanced FTTH cable making machinery provides measurable business value. It enables higher throughput and consistent optical performance with low attenuation. It also aligns with IEC 60794 and ITU-T G.652D / G.657 standards. Customers gain reduced labor costs and material waste through automation. Full delivery services cover installation and operator training.

The FTTH cable production line package contains fiber draw tower integration, a fiber secondary coating line, and a fiber coloring machine. It also includes SZ stranding line, fiber ribbone line, compact fiber unit assembly, cable sheathing line, armoring modules, and testing stations. Control and power specs often rely on Siemens PLC with HMI, operating at 380 V AC ±10% and modular power consumption up to roughly 55 kW depending on configuration.

Shanghai Weiye’s customer support model includes on-site commissioning by experienced engineers, remote monitoring, and rapid troubleshooting. It also offers lifetime technical support and operator training. Clients are commonly expected to coordinate engineer logistics as part of standard supplier practice when ordering from FTTH cable machine suppliers.

Key Takeaways

  • FTTH production line systems meet growing U.S. demand for fiber-to-the-home deployments.
  • Complete turnkey systems from Shanghai Weiye combine automation, standards compliance, and operator training.
  • Modular setups use Siemens PLC + HMI and operate near 380 V AC with up to ~55 kW power profiles.
  • Combined production modules cover drawing, coating, coloring, stranding, ribbon, sheathing, armoring, and testing.
  • Modern FTTH cable manufacturing systems reduces labor, waste, and improves optical consistency.
  • Service coverage includes on-site commissioning, remote diagnostics, and lifetime technical assistance.

SZ stranding lines

FTTH Cable Production Line Technology Explained

The fiber optic cable production process for FTTH calls for precise control at every stage. Manufacturers use integrated lines that combine drawing, coating, stranding, and sheathing. This approach boosts yield and speeds up market entry. It addresses the needs of both residential and enterprise deployments in the United States.

Below, we outline the core components together with technologies driving modern manufacturing. Each module must operate using precise timing together with reliable feedback. The choice of equipment shapes product quality, cost, and flexibility for various cable designs.

Core Components In Modern Fiber Optic Cable Manufacturing

Secondary coating lines apply dual-layer coatings, often 250 µm, using high-output UV curing. Tight buffering together with extrusion systems deliver 600–900 µm jackets for indoor as well as drop cables.

SZ stranding lines use servo-controlled pay-off together with take-up units to handle up to 24 fibers with accurate lay length. Fiber coloring machines employ multi-channel UV curing to mark fibers to industry color codes.

Sheathing and extrusion stations produce PE, PVC, or LSZH jackets. Armoring units add steel tape or wire for outdoor protection. Cooling troughs and UV dryers stabilize profiles before testing.

Evolution From Traditional To Modern Production Systems

Early plants used manual and semi-automatic modules. Lines were separate, featuring hand transfers as well as basic controls. Modern facilities move to PLC-controlled, synchronized systems with touchscreen HMIs.

Remote diagnostics and modular turnkey setups support rapid changeover between simplex, duplex, ribbon, and armored formats. This transition supports automated fiber optic cable production and reduces labor dependence.

Key Technologies Powering Industry Innovation

High-precision tension control, based on servo pay-off and take-up, keeps geometry stable during high-speed runs. Multi-zone temperature control using Omron PID and precision heaters ensures consistent extrusion quality.

High-speed UV curing together with water cooling improve profile stabilization while reducing energy rely on. Integrated inline testers measure attenuation, geometry, tensile strength, crush resistance, as well as aging data.

Function Typical Module Benefit
Optical fiber drawing Automated draw tower with tension feedback Uniform core size and low attenuation
Coating stage Dual-layer UV curing coaters Even 250 µm coating that improves durability
Fiber coloring Multi-channel fiber coloring machine Reliable color identification for field work
SZ stranding Servo-controlled SZ stranding line (up to 24 fibers) Stable lay length for ribbon and loose tube designs
Sheathing & extrusion Efficient extruders with multi-zone heaters PE, PVC, or LSZH jackets with tight dimensional control
Armoring Steel tape/wire armoring units Enhanced mechanical protection for outdoor use
Profile cooling & curing UV dryers and water troughs Quicker profile setting with fewer defects
Quality testing Inline attenuation and geometry measurement Live quality control and compliance reporting

Compliance using IEC 60794 together with ITU-T G.652D/G.657 variants is standard. Producers typically certify to ISO 9001, CE, and RoHS. These credentials enable diverse applications, from FTTH drop cable production to armored outdoor runs and data center high-density solutions.

Choosing cutting-edge fiber optic production equipment and modern manufacturing equipment helps firms meet tight tolerances. That decision enables efficient automated fiber optic cable production and positions companies to deliver on scale and quality.

Essential Equipment For Fiber Secondary Coating Line Operations

The secondary coating stage is critical, giving drawn optical fiber its final diameter and mechanical strength. It prepares the fiber for stranding and cabling. A well-tuned fiber secondary coating line controls coating thickness, adhesion, and surface quality. It protects the glass during handling.

Producers aiming for high-yield, high-speed fiber optic cable production must match material, tension, and curing systems to process requirements.

High-speed secondary coating processes rely on synchronized pay-off, coating heads, and UV ovens. Modern systems achieve high production rates while minimizing excess loss. Precise tension control at pay-off and winder stages prevents microbends and ensures consistent coating thickness across long runs.

Single and dual layer coating applications meet different market needs. Single-layer setups provide basic mechanical protection and a simple optical fiber cable production machine footprint. Dual-layer lines combine a harder inner layer with a softer outer layer to improve microbend resistance and stripability. This helps when fibers are prepared for connectorization.

Temperature control and curing systems are critical to final fiber performance. Multi-zone heaters and Omron PID controllers guide screw/barrel extruders to stable melt flow for LSZH or PVC compounds. UV curing ovens and water trough cooling stabilize the coating profile and reduce variation in excess loss; targets for high-quality single-mode fiber often aim for ≤0.2 dB/km at 1550 nm after extrusion.

Key components from trusted suppliers improve uptime and precision in an optical fiber cable production machine. Extruders such as 50×25 models, screws and barrels from Jinhu, and bearings from NSK are common. Motors from Dongguan Motor, inverters by Shenzhen Inovance, and PLC/HMI platforms from Siemens or Omron provide robust control and monitoring for continuous runs.

Operational parameters guide preventive maintenance as well as process tuning. Typical pay-off tension ranges from 0.4 to 1.5 N for fiber reels, while radiation as well as curing speeds are adjusted to material type together with coating thickness. A preventive maintenance cycle around six months keeps secondary coating processes stable as well as supports reliable fast-cycle fiber optic cable line output.

Fiber Draw Tower And Optical Preform Handling

The fiber draw tower is the core of optical fiber drawing. The line softens a glass preform in a multi-zone furnace. Then, it pulls a continuous strand with precise diameter control. That step sets the refractive-index profile together with attenuation targets for downstream processes.

Process control on the tower uses real-time diameter feedback and tension management. It helps prevent microbends. Cooling zones and closed-loop systems keep geometry stable during the optical fiber cable production process. Modern towers log metrics for traceability and rapid troubleshooting.

Output consistency supports single-mode fibers such as ITU-T G.652D and bend-insensitive types like G.657A1/A2 for FTTH networks. Draws routinely meet stringent loss figures. Excess loss after coating is kept at or below 0.2 dB/km for high-performance single-mode fiber.

Integration with secondary coating lines requires careful pay-off control. A synchronized handoff preserves alignment and tension as the fiber enters coating, coloring, or ribbon count stations. This link ensures the optical fiber drawing step feeds smoothly into cable assembly.

Equipment vendors such as Shanghai Weiye offer turnkey options. These include testing stations for attenuation, tensile strength, and geometric tolerances. These integrated features help manufacturers scale toward high-speed fiber optic cable production while maintaining ISO-level quality checks.

Feature Function Typical Target
Multi-zone furnace Consistent preform heating to stabilize glass viscosity Stable draw speed and refractive profile
Live diameter control Control core/cladding geometry while reducing attenuation ±0.5 μm tolerance
Cooling and tension control Protect fiber strength while preventing microbends Defined tension by fiber type
Automated pay-off integration Smooth transfer to coating and coloring Synced feed rates for zero-slip transfer
Inline test stations Verify loss, strength, and geometry Single-mode loss target of ≤0.2 dB/km after coating

Advanced SZ Stranding Line Technology For Cable Assembly

The SZ stranding method creates alternating-direction lays that cut axial stiffness and boost flexibility. That makes it ideal for drop cables, building drop assemblies, and any application that needs a flexible core. Manufacturers moving toward automated fiber optic cable manufacturing use SZ approaches to meet tight bend and axial tolerance specs.

Precision in the stranding stage protects optical performance. Advanced precision stranding equipment uses servo-driven carriers, rotors, and modular pay-off racks that accept up to 24 fibers. These systems deliver precise lay-length control together with allow quick reconfiguration for different cable types.

Automated tension control systems keep fibers within safe limits from pay-off to take-up. Servo pay-offs, capstans, and haul-off units maintain constant linear speed and target tensions. Typical fiber pay-off tension ranges from 0.4 to 1.5 N while reinforcement pay-offs run between 5 and 20 N.

Integration with a downstream fiber cable sheathing line streamlines production and reduces handling. Extrusion of PE, PVC, or LSZH jackets at 60–150 m/min syncs with stranding through a Siemens PLC. Cooling troughs and UV dryers stabilize the jacket profile right after extrusion to prevent ovality and reduce mechanical stress.

Optional reinforcement and armoring modules add strength without compromising flexibility. Reinforcement pay-off racks accept steel wires or FRP rods. Armoring units wrap steel tape or wire with adjustable tension to meet specific mechanical ratings.

Built-in output quality control prevents defects before cables leave the line. In-line geometry checks, fiber strain monitors, as well as optical attenuation measurement detect excess loss or mechanical strain caused by stranding or sheathing. These checks support continuous automated fiber optic cable manufacturing workflows as well as cut rework.

The combination of a robust sz stranding line, high-end precision stranding equipment, and a synchronized fiber cable sheathing line provides a scalable solution for manufacturers. This blend raises throughput while protecting optical integrity and mechanical performance in finished cables.

Fiber Coloring And Identification System Technology

Coloring and identification are critical in fiber optic cable production. Accurate color application minimizes splicing errors and accelerates field work. Modern equipment combines fast coloring with inline inspection, ensuring high throughput and low defect rates.

Today’s high-speed coloring technology supports multiple channels and quick curing. Machines can operate 8 to 12 color channels simultaneously, aligning with secondary coating lines. UV curing at speeds over 1500 m/min ensures color and adhesion stability for both ribbon and counted fibers.

The following sections discuss standards as well as coding prevalent in telecom networks.

Color coding adheres to international telecom standards for 12-color cycles together with ribbon schemes. That consistency aids technicians in installation and troubleshooting. Consistent coding significantly cuts field faults and accelerates network deployment.

Quality control integrates high-spec fiber identification systems into production lines. In-line cameras, spectrometers, as well as sensors detect color discrepancies, poor saturation, together with coating flaws. This PLC/HMI interface alerts to issues together with can pause the line for correction, safeguarding downstream processes.

Machine specifications are vital for uninterrupted runs together with material compatibility. Leading equipment accepts UV-curable pigments and inks, compatible with common coatings together with extrusion steps. Pay-off reels accommodating 25 km or 50 km spools ensure continuous operation on high-volume lines.

Supplier support is essential for US manufacturers adopting these technologies. Shanghai Weiye and other established vendors offer customizable channels, remote diagnostics, and onsite training. Such supplier support reduces ramp-up time and enhances the reliability of fiber optic cable production equipment.

Specialized Solutions For Fibers In Metal Tube Production

Metal tube and metal-armored cable assemblies provide robust protection for fiber lines. They are ideal for direct-buried and industrial applications. The controlled routing of coated fibers into metal tubes prevents microbends, ensuring optical performance remains within specifications.

Processes depend on precision filling and centering units. These modules, in conjunction with fiber optic cable manufacturing equipment, ensure concentric placement and controlled tension during insertion.

Armoring steps involve the use of steel tape or wire units with adjustable tension as well as wrapping geometry. That method benefits armored fiber cable line output by preventing compression of fiber elements. It also keeps reinforcement wires at typical diameters of ø0.4–ø1.0 mm.

Coupling armoring featuring downstream sheathing and extrusion lines results in a finished outer jacket made of PE, PVC, or LSZH. An optical fiber cable manufacturing machine must handle pay-off reels sized for reinforcement and align using sheathing tolerances.

Quality checks include crush, tensile, and aging tests to confirm the armor does not exceed allowable stress on fibers. Standards-based testing ensures long-term reliability in field conditions.

Turnkey solutions from established manufacturers integrate metal tube handling with SZ stranding and sheathing lines. These solutions include operator training and maintenance schedules to sustain throughput on fiber optic cable manufacturing equipment.

Buyers should consider compatibility using armored fiber cable line output modules, ease of changeover, together with service support for field upgrades. These factors reduce downtime as well as protect investment in an optical fiber cable line output machine.

Fiber Ribbon Line And Compact Fiber Unit Manufacturing

Advanced data networks require efficient assemblies that pack more fibers into less space. Manufacturers employ a fiber ribbon line to create flat ribbon assemblies for rapid splicing. That approach uses parallel processes and precise geometry to meet the needs of MPO trunking together with backbone cabling.

Advanced equipment ensures accuracy and speed in production. A fiber ribbon line typically integrates automated alignment, epoxy bonding, precise curing, and shear/stacking modules. In-line attenuation and geometry testing reduce rework, maintaining high yields.

Compact fiber unit line output focuses on tight tolerances and material choice. Extrusion together with buffering create compact fiber unit constructions using typical tube diameters from 1.2 to 6.0 mm. Common materials include PBT, PP, as well as LSZH for durability together with flame performance.

High-density cable solutions aim to enhance rack together with tray efficiency in data centers. By increasing fiber count per unit area, these designs shrink cable diameter as well as simplify routing. They are compatible using MPO trunking and high-count backbone systems.

Production controls and speeds are critical for throughput. Current lines can reach up to 800 m/min, depending on configuration. PLC as well as HMI touch-screen control enable quick parameter changes and synchronization across multiple lines.

Quality and customization remain key differentiators for manufacturers like Shanghai Weiye. Electronic monitoring, customizable ribbon counts, stacking patterns, and turnkey integration with sheathing and testing stations support bespoke high-speed fiber cable production line requirements.

Production Feature Ribbon Line Compact Fiber Unit Benefit for Data Centers
Line speed Up to roughly 800 m/min Around 600–800 m/min Greater throughput for large-scale deployments
Main production steps Automated alignment, bonding, and curing Extrusion, buffering, tight-tolerance winding Improved geometry consistency with lower insertion loss
Primary materials Specialty tapes and bonding resins PBT, PP, and LSZH jackets/buffers Durable performance and safety compliance
Inspection Inline attenuation and geometry checks Precision dimensional control with tension monitoring Fewer field failures and quicker deployment
System integration Integrated sheathing with splice-ready stacking Modular compact units for dense cable solutions More efficient MPO trunk and backbone deployment

Optimizing High-Speed Internet Cables Production

Efficient high-output fiber optic cable manufacturing relies on precise line setup and strict process control. To meet US market demands, manufacturers must adjust pay-off reels, extrusion dies, as well as tension systems. That helps ensure optimal output for flat, round, simplex, and duplex FTTH profiles.

FTTH Application Cabling Systems

FTTH cabling systems must accommodate various drop cable types while maintaining consistent center heights, like 1000 mm. Production lines for FTTH include 2- and 4-reel pay-off options. They also feature reinforcement pay-off heads for enhanced strength.

Extruder models, such as a 50×25, control jacket speeds between 100 together with 150 m/min, depending on LSZH or PVC. Extrusion dies for 2.0×3.0 mm profiles guarantee reliable jackets for field installation.

Quality Assurance In The Fiber Pulling Process

Servo-controlled pay-off and take-up units regulate fiber tension between 0.4–1.5 N to prevent excess loss. Inline systems conduct fiber pull testing, attenuation checks, mechanical tensile tests, and crush and aging cycles. These tests verify performance.

Key control components include Siemens PLCs and Omron PID controllers. Motors from Dongguan Motor and inverters from Shenzhen Inovance ensure stable operation and easier maintenance.

Meeting Optical Fiber Drawing Industry Standards

A well-tuned fiber draw tower produces fibers that meet ITU-T G.652D and G.657 standards. The goal is to achieve ≤0.2 dB/km excess loss at 1550 nm for high-quality single-mode fiber.

Choosing the best equipment for FTTH cables involves evaluating speed, customization, warranty, as well as local after-sales support. Top FTTH cable line output line manufacturers offer turnkey layouts, remote monitoring, as well as operator training. This cuts ramp-up time for US customers.

Closing Summary

Advanced FTTH cable making machinery integrates various components. These include fiber draw towers, secondary coating, coloring lines, SZ stranding, and ribbon units. It further contains sheathing, armoring, as well as automated testing for consistent high-output fiber manufacturing. A complete fiber optic cable line output line is designed for FTTH as well as data center markets. This system enhances throughput, keeps losses low, together with maintains tight tolerances.

For U.S. manufacturers and system integrators, partnering with reputable suppliers is key. They should offer turnkey systems with Siemens or Omron-based controls. This includes on-site commissioning, remote diagnostics, and lifetime technical support. Companies like Shanghai Weiye Optic Fiber Communication Equipment Co provide integrated solutions. These systems simplify automated fiber optic cable manufacturing and reduce time to production.

Technically, ensure line configurations adhere to IEC 60794 and ITU-T G.652D/G.657 standards. Verify tension and curing settings to meet excess loss targets, such as ≤0.2 dB/km at 1550 nm. Adopt preventive maintenance cycles of roughly six months for reliable 24/7 operation. When planning a new FTTH cable production line, first evaluate required cable types. Collect product drawings and standards, request detailed equipment specs and turnkey proposals, and schedule engineer commissioning and operator training.

Ribbon Cohesion on a Fiber Ribbon Line

Is It Possible That the machines producing fiber optic cable production machinery act as the unseen force that ultimately delivers true gigabit access to every American home? This article examines the recent breakthroughs in FTTH Cable Production Line Technology. These advancements are revolutionizing broadband network infrastructure and speeding up fiber to the home technology across the United States.

Fiber Secondary Coating Line

Fiber Secondary Coating Line

Fiber Secondary Coating Line

Modern advancements in automation, precision engineering, and AI-driven inspection are substantially lowering production costs and enhancing quality. This synergy makes high-speed internet technology more dependable and simpler to deploy for service providers and municipalities.

Global optical cable output now exceeds hundreds of millions of kilometers annually. This surge is driven by 5G deployments, hyperscale data centers, and the growing demand for streaming and remote work. The subsequent sections will delve into automation and Industry 4.0, the use of low-loss materials, AI quality control, innovative cable designs such as bend-insensitive fiber and flat drop microcables, and the pursuit of sustainability in production lines.

Telecommunications manufacturing, network planning, and procurement professionals will gain valuable insights. These insights relate to selecting the right fiber optic cable production machinery and optimizing processes. They are designed to meet regional deployment needs and future bandwidth growth.

FTTH Cable Production Line Technology

The term encompasses the machinery, control systems, and materials transforming optical preforms into deployable fiber cables. It covers fiber drawing and coating, SZ stranding, ribbon formation, extrusion of jackets, armoring, taping, automated testing, and final take-up systems. Each step’s precise control defines the fiber optic cable production process, ensuring consistent performance.

The manufacturing chain demands stringent tolerances. SZ stranding systems align dozens of strands with micron-level tension precision. Extrusion lines employ servo-driven extruders and laser micrometers to maintain jacket thickness within ±0.02 mm. Such precision minimizes variability, lowering attenuation and making field splicing easier.

Standards and regulatory frameworks significantly influence manufacturing decisions. Compliance with ITU-T recommendations, such as G.657, and regional fire codes like CPR in Europe, is essential. Meeting these standards ensures products align with the broader broadband network infrastructure.

Quality in production directly impacts network economics and service delivery. Lower attenuation and consistent geometry reduce splice loss and extend reach. This enhances reliability for carriers, ISPs, and utilities, while lowering the total cost of ownership for FTTH deployments. The growing demand for symmetrical multi-gigabit services, 5G backhaul, and data center interconnect is driving the scale-up of modern lines.

Comparing key process components and tolerances reveals their impact on output and quality.

SZ Stranding Line

Process Component Standard Control Impact on Performance
Fiber drawing & coating ±1°C temperature control; coating concentricity ±5 µm Stable fiber profile; lower bending-related loss
SZ stranding & ribbon formation Micron-level tension regulation; synchronization at 0.5 ms Consistent fiber pitch; reliable splice and connector behavior
Extrusion & jacket thickness Laser micrometer feedback; tolerance of ±0.02 mm Uniform protection; more predictable installation handling
Armoring & taping Servo feed rate; layer alignment control Better crush resistance; meets aerial and underground specs
Automated testing & take-up OTDR and insertion loss checks at line speed; tension-controlled winding Complete quality traceability; lower rework and fewer failures in the field

Manufacturers like Corning, Prysmian Group, and Sumitomo Electric focus on tighter process control to meet operator expectations. Continuous advancements in the fiber optic cable production process enable networks to scale while maintaining performance in the last mile of broadband network infrastructure.

Automation And Industry 4.0 In Fiber Optic Cable Production

Factory floors for fiber optic cable production machinery now mirror advanced manufacturing plants from other industries. Smart controls, synchronized stages, and data-driven decision making raise output and protect quality. These shifts shorten commissioning time for new product families. They let telecommunications equipment manufacturers pivot between armored aerial lines and microcable runs with minimal downtime.

Smart machinery and PLC integration

Programmable logic controllers coordinate stranding frames, ribbon formers, and take-up units to keep tension within sub-0.01mm windows. Servo-driven extrusion coupled with laser micrometers enforce ±0.02mm jacket thickness. The result is fewer rejects, less rework, and consistent optical performance on every reel.

Edge processing and process coordination

Local edge servers ingest terabytes of telemetry each day. They drive low-latency closed-loop adjustments and push immediate alerts when deviations occur. This approach keeps optical fiber cable equipment running at peak efficiency. It supports real-time quality assurance during long production runs.

AGVs, material handling, and workflow gains

Automated Guided Vehicles move heavy cable drums with millimeter-level repeatability. Laser-navigated AGVs reduce manual handling injuries and speed material flow between extrusion, curing, and drum stations. This automation lowers labor costs while raising throughput on ftth cable production line technology setups.

Advantages for manufacturers and supply networks

  • Greater throughput with repeatable outcomes
  • Quicker prototyping and a shorter path to market
  • Reduced labor exposure and lower operating cost
  • Better integration between optical fiber cable equipment and enterprise systems

Industry ecosystem and adoption

Leading telecommunications equipment manufacturers pair PLCs with robotic arms, AGVs, and industrial IoT stacks to reach Industry 4.0 goals. This integration creates a resilient production base. It is able to adapt as demand shifts toward denser, more complex FTTH offerings.

Precision Engineering Breakthroughs For Lower Attenuation

Advances in materials and mechanical design are driving down loss in modern fiber lines. Engineers pair ultra-low loss fiber with tighter coating control to reduce intrinsic and bending attenuation. These gains matter to network operators who want longer spans and fewer amplifiers in high-speed internet technology deployments.

The fiber optic cable production process now favors smaller coated diameters such as 180µm and 160µm. These sizes let manufacturers increase fiber count and build denser microcables without sacrificing handling or optical stability.

Low-Loss Glass And Advanced Coatings

Manufacturers use improved glass formulations that lower Rayleigh scattering and reduce baseline attenuation. Ultra-low loss fiber variants extend reach for long-haul and high-capacity links while easing repeaters and amplifier requirements.

Coating chemistry has progressed too. UV-cured acrylate systems cut microbending loss by roughly 40% compared with earlier generations. That performance drop helps maintain signal integrity in cramped ducts and tight bends common in FTTH and 5G backhaul networks.

Central Strength Members And Mechanical Design

Mechanical design updates center on robustness and dimensional control. Fiber-reinforced plastic (FRP) rods with tensile strengths near 1.2 GPa serve as central strength members. They limit elongation during pulling and boost crush and bending resilience.

Water-blocking advances use swellable yarns and grease-free gel compounds to achieve near-complete moisture resistance. These measures protect optical paths and raise in-service reliability for cable installations in challenging environments.

These precision engineering steps integrate directly into fiber optic cable manufacturing workflows. When the production line aligns glass, coating, and mechanical specs, attenuation falls and networks gain reliability. That alignment shortens time to service for operators deploying modern broadband and high-speed internet technology.

Quality Control 4.0 And AI-Powered Inspection

Smart factories for fiber optic cable production now embed inspection systems that run continuously. These systems combine machine vision, machine learning, and automated testers to watch every reel and spool. The result is tighter feedback during the fiber optic cable production process and fewer surprises in the field.

AI models score coating uniformity, microbends, and surface defects at line speed. They cross-reference process telemetry from fiber optic cable production machinery and predict deviations hours before a reel moves to final spooling. This allows for in-line adjustments without stopping the line.

Automated OTDR integration performs 100% attenuation testing on every length. Modern OTDR systems using 1550nm sources map loss across reels and flag changes as small as 0.01 dB/km. Inline OTDR logs feed edge analytics for rapid root-cause tracing when a batch shows anomalies.

Robotic bend-radius simulators apply repeated stress cycles while monitoring macrobend loss. These testers validate compliance with ITU-T G.657 and customer bend specifications by running controlled bends at multiples of the cable diameter. Test outcomes are tied to batch IDs for traceability.

Thermal cycling chambers stress jackets and splices across wide temperature ranges. Environmental tests up to +85°C and down to -60°C confirm stability for extreme climates. Automated logs record each chamber run and link results to production lots.

Quality control 4.0 reduces returns and field failures by making 100% in-line testing routine. Edge analytics and OTDR integration shorten diagnosis times and improve regulatory compliance. Broadband operators see fewer truck rolls and better lifecycle performance for FTTH networks.

Cable Design Innovations For FTTH Deployments

New cable designs address common field challenges in fiber to the home technology. Engineers focus on durability, space economy, and speed of activation. These trends reduce installation time and lower long-term operational costs.

Bend-Insensitive Fiber Benefits For MDUs And Tight Routing

Bend-insensitive fiber maintains signal strength when routed around corners and through confined spaces. ITU-T G.657 compliant fibers minimize attenuation at tight radii, protecting links in multi-dwelling units and behind baseboards. Prysmian’s BendBright family and BendBrightXS exemplify how smaller coated diameters facilitate routing without compromising optical performance.

Flat Drop And Microcable Options For Flexible Deployments

Flat drop cable remains a preferred choice for aerial self-support, duct installs, and direct burial in North America. Its profile accommodates narrow pathways and enhances aerial spans with appropriate clamps. High-fiber-count flat drops necessitate enhanced radial strength and more robust hardware for longer spans.

Microcable technologies reduce outside plant profiles to 8 mm or less. Microcables and air-blown systems enable capacity addition inside existing ducts and congested corridors. These approaches reduce civil works, lower labor costs, and facilitate incremental network growth for urban and campus builds.

Pre-Connectorized Solutions To Speed Field Activation

Pre-connectorized solutions offer factory-terminated, plug-and-play assemblies that minimize field fusion and connector errors. Hardened outdoor connectors and vendor offerings like Prysmian’s ezDROP simplify mass rollouts and enhance first-pass yield. Service teams experience fewer truck rolls and faster service turn-up for smart city and 5G edge projects.

Cable Design Core Advantage Typical Use Case Deployment Factor
Bend-insensitive optical fiber Reliable operation at tight bend radii Multi-dwelling units, indoor routing, compact pathways Use ITU-T G.657 fiber variants for indoor routing
Flat drop fiber cable Multiple deployment modes Aerial service drops, direct burial, duct installs Apply suitable clamps and radial-strength hardware
Microcable technologies Compact profile with scalable capacity Microduct installations, crowded urban ducts Compatible blower tools are required for air-blown systems
Factory-connectorized solutions Faster service turn-up and reduced errors Mass deployments, rapid service turn-up Standardized connector interfaces should be planned for

Sustainability And Energy Efficiency In Production Lines

Manufacturers in the fiber optic cable industry are embracing greener practices to reduce costs and meet consumer demands. Facilities prioritizing sustainable production witness improvements in operational efficiency and brand reputation. These advancements impact power systems, cooling, raw materials, and waste management.

Power recovery strategies are becoming prevalent on extrusion lines and take-up reels. Regenerative braking on motor-driven spools returns power to the grid, thereby lowering net consumption. Studies indicate that energy recovery can reduce drive energy use by up to 32 percent in retrofitted reels.

Closed-loop cooling and chiller-less extrusion systems are reducing water demand. Adiabatic cooling can decrease water use by as much as 75 percent, particularly beneficial in water-scarce areas. Plants employing closed-loop cooling systems, in conjunction with heat exchangers, maintain temperature control while reducing utility expenses.

Recyclable jacket materials are transforming the disposal of cables. New polypropylene-based and modified polymer compounds meet mechanical and fire-safety standards, enabling higher recycling rates. Suppliers like Borealis and LyondellBasell are developing compounds that support the circular economy in cable jackets.

Process optimization minimizes scrap before recycling. Precision extrusion, in-line laser measurement, and real-time analytics reduce off-spec runs. Digital twins enable engineers to refine parameters, enhancing batch yields and reducing material waste.

Regulatory pressures and corporate ESG goals are compelling operators to favor vendors with transparent sustainability metrics. Municipal procurement teams and large network operators increasingly consider lifecycle impacts when selecting suppliers.

Operational Area Typical Improvement Main Benefit
Regenerative drives on take-up reels Energy reduction up to 32% Lower electricity costs and reduced peak demand
Closed-loop cooling and adiabatic systems Approximately 75% reduction in water use Lower water expenses and better compliance in arid areas
Recyclable jacket materials Greater post-consumer recyclability Stronger circular economy support and easier disposal
Digital twins and in-line inspection Noticeable double-digit reductions in scrap and off-spec output Better yield, less material waste
Sustainability reporting and certifications Better standing in procurement Stronger appeal to network operators

Implementing these measures enhances the resilience of fiber optic cable manufacturing. It leads to lower lifecycle costs and easier compliance. Manufacturers integrating energy recovery and recyclable jacket materials position themselves for growth in the green procurement market.

Emerging Technologies Shaping Cable Manufacturing

New technologies are transforming the design and operation of fiber optic cable production machinery. These innovations expedite commissioning, diminish prototyping cycles, and empower manufacturers to test process alterations without halting production.

Digital twins create virtual replicas of entire production lines and novel cable designs. Engineers at Corning and Prysmian leverage these models to validate footprint, material flow, and layout before physical construction. Studies indicate commissioning can be up to 60% swifter when teams execute virtual scenarios and optimize layouts beforehand.

Digital twins facilitate expedited R&D for bespoke items such as armored variants and anti-rodent jackets. Virtual testing minimizes the necessity for physical prototypes and accelerates market entry. Teams can simulate process modifications, observe material interactions, and refine equipment parameters in a risk-free milieu.

AI systems introduce predictive capabilities on the factory floor. Machine learning scrutinizes 50+ parameters to forecast failures and quality deviations hours in advance. This AI predictive maintenance lessens unplanned downtime and elevates overall equipment effectiveness for high-volume lines.

Manufacturers like Siemens and ABB integrate AI with edge computing, enabling models to operate proximal to machines. Alerts prompt targeted inspections, spare part staging, and corrective actions before a fault halts production. This strategy maintains yield and shortens mean time to repair.

Quantum fiber sensing and distributed monitoring extend capabilities beyond production to the deployed cable. Embedded Brillouin and distributed acoustic sensing provide continuous strain and temperature data across extensive spans.

Integration of quantum fiber sensing enhances network diagnostics and supports structural health monitoring. Field teams acquire actionable insights when sensing data is linked to manufacturing records and test logs. This connection enables tracing anomalies to specific production batches.

Combined workflows—digital twins plus AI predictive maintenance—accelerate both commissioning and product development. Manufacturers embracing these tools can respond more swiftly to market fluctuations and deliver higher-value, differentiated cables.

Market-Driven Production Adaptations And Regional Needs

The global demand for fiber access compels manufacturers to adapt their production lines to local requirements. Regional fiber optic cable manufacturing now emphasizes durability, density, and safety. Plants employ modular equipment, enabling swift transitions between product families and meeting specific operator needs without significant delays.

In North America, networks predominantly opt for aerial routes and robust outside-plant solutions. Producers concentrate on creating armored aerial cables with enhanced breaking strength, corrosion-resistant armor, and simplified pole-mount installation. These designs withstand wind, ice, and long span stresses typical of utility corridors.

North American Priorities: Aerial And Armored Designs

Armored aerial cables are engineered for enduring reliability on poles and open spans. They boast 1,200 lb or greater tensile ratings and integrated steel or aluminum armoring to safeguard fibers against mechanical damage. Manufacturers deploy modular armoring units and rapid testing rigs, enabling mass production of these variants.

APAC And Europe: High-Density Microcables And Regulatory Compliance

In APAC, the scarcity of space and the need for dense builds drive demand for high-density microcables. These cables feature compact stranding towers and reduced-diameter fiber stacks, allowing for more fibers per duct. They significantly reduce civil costs by facilitating quicker overbuilds and easier microtrenching.

Europe mandates strict regulatory compliance for buildings and public spaces. Producers offer halogen-free, flame-retardant jackets that meet CPR classes like B2ca. Compliance testing is integrated into production lines, ensuring products meet fire-safety rules for indoor and outdoor applications promptly.

Across regions, the ability to adapt production is paramount. Compact stranding towers, modular extrusion and armoring units, and rapid prototyping enable factories to switch from armored aerial cables to microcable runs in mere hours. This flexibility allows operators to fulfill unique specifications while adhering to local codes.

Case Studies And Manufacturer Spotlight: Shanghai Weiye OFC Equipment

Shanghai Weiye OFC Equipment has solidified its reputation as a leading telecommunications equipment manufacturer. They cater to the FTTH and broader fiber markets. Their optical fiber cable equipment boasts advanced features, including SZ stranding, ribbon production, and extrusion with servo control. This ensures tight tolerances and high yields.

Their machinery for fiber optic cable production is equally impressive. It includes tape armoring units, automated take-up reels with regenerative drives, and integrated OTDR and vision inspection stations. These systems support various applications, such as bend-insensitive fiber, microcables, and pre-connectorized solutions. These are crucial for FTTH, 5G backhaul, and dense urban deployments.

Quality and sustainability are integral to their offerings. They employ OTDR testing, AI-powered inspection, and robotic bend simulators to meet QC 4.0 standards. Additionally, energy recovery options and closed-loop cooling reduce operating costs and scrap. Modular designs with AGV and edge computing support enable rapid reconfiguration and digital twin commissioning, catering to U.S. manufacturers and contract producers.

For operators in the United States, investing in Shanghai Weiye OFC Equipment can significantly enhance production capabilities. It ensures compliance with strict attenuation and mechanical specifications. This accelerates the introduction of new cable families, vital for broadband expansion. The company’s systems harmonize technical performance with practical manufacturing requirements.

FAQ

Q: What Advances Define Modern FTTH Cable Production Line Technology?

A: Modern FTTH cable production lines integrate high-precision mechanical systems with servo-driven extrusion. They utilize SZ stranding and ribbon machines, along with automated take-up reels. These systems also include integrated OTDR and AI-driven vision inspection, PLC orchestration, AGV material handling, and edge computing. Such advancements enable micron-level tension control and ±0.02mm jacket thickness tolerances. They achieve 95%+ automation and 100% in-line testing, reducing attenuation, scrap, and time-to-market.

Q: How Do You Define The Scope Of FTTH Cable Production Line Technology?

A: FTTH cable production line technology includes the machinery, process controls, and materials for fiber-to-the-home networks. It includes optical fiber drawing and coating, SZ stranding, and ribbon formation. Extrusion of inner and outer jackets, armoring or taping modules, and automated take-up and drum handling are also part of it. In-line optical and mechanical testing, along with the software stack—PLCs, edge servers, and industrial IoT—are integral to the process.

Q: Why Does Production-Line Quality Matter For Broadband Network Infrastructure?

A: Production-line quality directly impacts attenuation, splice loss, mechanical robustness, and long-term reliability. High-precision manufacturing minimizes intrinsic and macrobending losses. It extends reach, lowers field interventions, and improves first-pass yields. For carriers and ISPs, this translates to fewer truck rolls, lower total cost of ownership, and higher service availability for high-speed internet, 5G backhaul, and symmetrical multi-gigabit home services.

Q: What Role Do PLCs And Smart Machinery Play In Industry 4.0 Production Lines?

A: Programmable logic controllers (PLCs) provide deterministic synchronization across SZ stranding, ribbon forming, and take-up units. They enable sub-0.01mm tension precision, closed-loop extrusion control, automated recipe changes, and safety interlocks. When combined with robotic arms and automated armoring modules, PLCs form the backbone of Industry 4.0 production. They drive repeatability and high throughput with minimal human intervention.

Q: How Are AGVs And Edge Computing Used On Modern Cable Production Floors?

A: Laser-navigated AGVs move heavy drums and material spools with high positioning accuracy. Industry examples show 1,200kg capacity and sub-5cm placement. Edge computing processes terabytes of telemetry locally, delivering low-latency analytics and real-time quality alerts. Together, AGVs and edge computing improve material flow, reduce manual handling risks, and enable rapid correction of process deviations.

Q: What Precision Engineering Improvements Reduce Optical Attenuation?

A: Improvements include ultra-low-loss (ULL) glass formulations and advanced UV-cured acrylate coatings. These coatings cut microbending losses. Smaller coated diameters (e.g., 160–180µm) enable denser cable designs. Tight control of drawing tension, coating cure profiles, and extrusion concentricity—monitored by laser micrometers and closed-loop controls—lowers intrinsic loss and fluctuation across production reels.

Q: How Do Central Strength Members And Mechanical Design Affect Cable Performance?

A: Mechanical designs incorporating fiber-reinforced plastic (FRP) rods or high-strength central members control elongation during installation. They resist crush and bending, protecting fiber glass from strain. Proper selection of strength elements and buffer constructions reduces installation-induced loss, improves long-term reliability, and supports aerial or duct deployments with demanding mechanical requirements.

Q: What Does “QC 4.0” Mean And How Is It Implemented?

A: QC 4.0 describes a fully instrumented, data-driven quality-control regime. It includes 100% in-line testing, AI-powered vision inspection, automated OTDR mapping, robotic bend tests, and environmental chambers integrated into the production workflow. Edge analytics, traceable test logs, and predictive models enable rapid root-cause analysis, minimize returns, and ensure compliance with ITU-T and operator specifications.

Q: How Is OTDR Testing Integrated Into Production And What Sensitivity Can It Achieve?

A: Automated OTDR stations are integrated inline or at take-up to perform full-length attenuation mapping. They use dual-wavelength sources (including 1550nm). Modern setups can detect variations down to 0.01 dB/km, map localized defects, and tie results to batch IDs for traceability. This enables manufacturers to flag and quarantine reels before shipment, improving field reliability.

Q: What Are Robotic Bend-Radius Simulators And Thermal Cycling Chambers Used For?

A: Robotic bend-radius simulators apply repeated controlled bends and record macrobend loss to verify compliance with ITU-T G.657 and customer specs. Thermal cycling chambers run jackets and assemblies through −60°C to +85°C cycles to validate dimensional stability, jacket adhesion, and splice performance under extremes. Automated test logs provide traceable evidence for operator and regulatory requirements.

Q: What Cable Design Innovations Are Most Relevant To FTTH Deployments?

A: Key innovations include bend-insensitive fiber (BIF) for tight routing in MDUs and indoor paths. Flat drop and high-fiber-count flat assemblies are used for aerial and direct-burial North American use cases. Microcables and air-blown systems are for duct-constrained environments. Pre-connectorized assemblies speed field activation and reduce termination errors.

Q: Why Is Bend-Insensitive Fiber Important For MDUs And Tight Routing?

A: Bend-insensitive fiber maintains low loss under tight radii and repeated handling. It is crucial in multi-dwelling units, plenum runs, and behind baseboards. ITU-T G.657-compliant fibers help prevent macrobending loss during installation and reduce service calls related to routing-induced degradation. They support denser routing with fewer installation constraints.

Q: How Do Flat Drop Cables And Microcables Differ In Deployment Benefits?

A: Flat drop cables offer flexible aerial and direct-burial deployment with compact profiles suited to service drops. Microcables (≤8mm) and microduct systems excel in congested ducts and enable incremental capacity growth via air-blown installation. Choice depends on regional deployment practice, span requirements, and operator preferences.

Q: What Advantages Do Pre-Connectorized Solutions Provide?

A: Factory-terminated, hardened pre-connectorized assemblies reduce field splicing, eliminate human termination variability, and speed up service activation. They improve first-pass yield. Products like hardened OptiTap-style connectors and vendor pre-terminated drops support rapid mass-deployment strategies and lower workforce training needs.

Q: How Are Energy Recovery And Cooling Innovations Improving Sustainability?

A: Regenerative drives on take-up reels and motor assemblies can capture braking energy, reducing net consumption by industry-reported amounts (example: up to ~32%). Chiller-less or adiabatic extrusion cooling reduces water use by up to 75%. These measures lower operational cost, reduce water consumption, and align production with corporate sustainability targets.

Q: Are Recyclable Jacket Materials And Waste Reduction Practical For Production?

A: Yes. Recyclable compounds such as specially formulated polypropylene-based jackets can meet mechanical and flame performance while improving end-of-life recycling. Precision extrusion and in-line inspection reduce scrap rates. Combined with material-efficient tooling and digital-twin optimization, manufacturers can materially lower waste and support circular-economy goals.

Q: What Role Do Digital Twins Play In Cable Manufacturing?

A: Digital twins create virtual replicas of production lines and cable designs to simulate process changes and validate material flow. They accelerate commissioning. Industry estimates show commissioning and prototyping time reduced significantly (case examples up to ~60%). Digital twins also support offline testing of recipe changes and faster roll-out of new product families.

Q: How Does AI Enable Predictive Maintenance And Quality Prediction?

A: Machine learning models trained on dozens of production parameters can forecast equipment faults hours in advance and predict quality drift. Predictive maintenance reduces unplanned downtime, improves OEE, and allows planned service windows. AI-driven quality models provide early alerts for deviations that would otherwise produce rejects or field failures.

Q: What Is The Significance Of Quantum And Distributed Sensing Integration In Cables?

A: Embedding distributed sensing capabilities—such as Brillouin-based strain sensing and distributed acoustic sensing (DAS)—adds network-level telemetry for structural health monitoring, intrusion detection, and environmental diagnostics. Integrating sensing into cable designs enables added-value services and improved operational visibility for carriers and critical infrastructure owners.

Q: How Do Production Lines Adapt To Regional Market Needs (North America, APAC, Europe)?

A: Lines are modular and reconfigurable to meet regional priorities. North America focuses on robust aerial and armored designs with higher breaking-strength requirements for pole deployments. APAC emphasizes high-density microcables and compact stranding for dense urban rollouts. Europe prioritizes halogen-free flame-retardant jackets and CPR fire-class compliance. Modular stranding towers, quick-change extrusion heads, and configurable armoring units enable fast changeovers.

Q: What Manufacturing Equipment Is Essential To Support Varied FTTH Product Families?

A: Essential equipment includes SZ stranding machines (dozens to hundreds of fibers with micron-level tension control), ribbonization lines, servo-driven extruders with laser micrometers, tape or armor-wrapping stations, automated take-up reels with regenerative drives, inline OTDR and AI vision inspection, AGV drum handling, and edge computing/PLC orchestration for Industry 4.0 integration.

Q: How Do Manufacturers Ensure Compliance With Standards Like ITU-T G.657 And Regional Safety Codes?

A: Compliance is ensured via precise material selection (bend-insensitive fiber types), controlled production recipes, automated in-line tests (OTDR, macrobend testers), and environmental qualification (thermal cycling, flame tests). Traceable test logs, batch IDs, and documented QC protocols align production outputs with ITU-T recommendations and regional regulations such as CPR classifications in Europe.

Q: What Benefits Can U.S. Manufacturers Expect From Equipment Suppliers Like Shanghai Weiye OFC Equipment?

A: Suppliers like Shanghai Weiye provide modular, Industry 4.0-ready production machinery—SZ stranding, ribbon lines, precision extrusion with closed-loop controls, AI inspection modules, and integrated OTDR testing. This enables U.S. contract manufacturers and in-house producers to scale FTTH output, maintain tight attenuation and mechanical tolerances, adopt sustainability options (energy recovery, closed-loop cooling), and shorten time-to-market for variants such as armored aerial, flat drop, microcable, and pre-connectorized assemblies.

Q: How Do In-Line AI Inspection Systems Detect Subtle Defects At Production Speed?

A: AI-powered machine vision inspects coating uniformity, surface defects, and microbends using high-resolution cameras and convolutional models trained on labeled defect libraries. Models correlate dozens of parameters—diameter variance, coating texture, micro-crack signatures—to predict deviations hours before they become out-of-spec reels. This enables automated rejection, parameter adjustment, and reduced downstream field failures.

Q: What Testing Sensitivity And Traceability Are Achievable For Attenuation And Mechanical Validation?

A: Modern production lines integrate automated OTDR systems capable of resolving 0.01 dB/km changes, robotic bend simulators for repeated macrobend stress testing, and thermal chambers for extreme environment validation. Test results are stored with batch and reel identifiers in edge or cloud databases, providing full traceability for operator acceptance, regulatory audits, and customer service diagnostics.

Q: How Do Production Innovations Translate Into Market Outcomes For Network Operators?

A: Innovations in manufacturing yield lower-loss fibers, denser cable designs, and factory-terminated assemblies that reduce installation time and errors. Operators benefit from higher service reliability, fewer truck rolls, lower lifecycle costs, and faster rollout of symmetrical multi-gigabit services. These outcomes support widespread FTTH adoption, 5G backhaul capacity, and scalable connectivity for smart cities and hyperscale data center interconnects.

Related: Quality-Control Checklist for Every Fiber Draw Tower Pull